The raw materials for flux-cored wire come down to two things: a low-carbon steel strip that gets formed into the outer sheath, and a powdered core made from minerals, ferroalloys, and metal powders blended for a specific job. The steel does the structural work and carries the current; the powder does the chemistry — shielding the puddle, stabilizing the arc, cleaning the metal, and tuning the properties of the finished weld. Everything else you have heard about this wire, from deposition rates to outdoor performance, flows from how well those two ingredient lists were chosen and mixed.
A fabricator I work with learned that lesson the expensive way about four years ago. He runs a small structural shop doing railings, frames, and the occasional repair job, and he buys consumables the way most small shops do — by the spool, on price, from whoever has stock. A batch of bargain flux-cored wire showed up in the shop, and for the first two or three days nobody complained. Then the complaints started. The wire fed with a stutter on vertical welds. The slag came off in tenacious patches instead of lifting in one piece. Some beads had a fine rash of surface pores that the same machine, same gas, and same operator had never produced before. They went through a week blaming the welder, the drive rolls, and the liner, replaced parts that did not need replacing, and lost two days of output.
The fix took an afternoon. The owner pulled a spool of the wire he had used for years, ran the identical joint with the identical settings, and every symptom disappeared. The bargain spool went in the scrap bin. Nobody ever analyzed the chemistry of that cheap wire — they did not need to. The behavior told the story: an unstable arc, a slag that would not release, and a weld pool that could not decide what it was doing are all symptoms of a flux formulation that was never engineered for the job printed on the label.
That story is the reason this subject matters beyond the manufacturing floor. When you buy a spool of flux-cored wire, you are buying a chemical package as much as you are buying metal. The ingredient list determines whether the wire burns smoothly at your settings, whether the slag peels, whether the weld is tough in winter, whether it survives a salt spray, and whether the beads come out clean after one pass. Understanding what is inside the tube — and why the raw materials matter — turns wire selection from a price comparison into a technical decision. It also explains a lot of the frustrations that get blamed on the welder or the machine when the real problem shipped from a factory.
This article walks through every category of raw material that goes into flux-cored wire: the steel strip, the ferrous powders, the non-ferrous additions, the minerals that make up the flux, the binders and coatings, and the testing and sustainability questions around sourcing them. It closes with a practical checklist for judging wire quality at the counter, because most people reading this will never visit a wire plant — but everyone reading this buys spools.
What Flux-Cored Wire Actually Is
Before the ingredients make sense, the architecture has to. Flux-cored wire — also called tubular wire or cored wire — is a composite consumable. A flat strip of steel is rolled into a tube around a continuous column of powder, the seam is welded shut, and the tube is drawn down to the final diameter you feed through the gun. The result looks like solid wire from the outside, but cut a cross-section and the powder core is plain to see running down the center.
That tubular structure is the whole trick. Because the shielding chemistry travels inside the wire rather than arriving entirely through an external gas bottle, cored wire can do things solid wire cannot: generate its own local shield, carry alloying elements directly into the puddle in powder form, deposit metal faster, and run in positions where a fluid solid-wire puddle would sag. The two broad families follow from that design. Self-shielded flux-cored wire protects the arc using gases generated by the core itself, so no bottle is needed. Gas-shielded flux-cored wire — often called dual shield — relies on an external gas, typically CO2, while the core handles slag, alloying, and arc behavior. Both types share the same raw-material categories; they differ in the ratio and the recipe.
The Sheath: Steel Strip
The outer skin starts as coil of steel strip, most often a low-carbon rimmed or semi-killed steel chosen for formability and consistent drawing behavior. The strip has to survive being bent into a tight tube at high speed, resistance-welded along the seam, and then pulled through a series of dies that reduce the diameter by a large fraction without cracking the weld seam. If the strip chemistry drifts hard, or the coil has inconsistent hardness, the tube-forming line will tell you about it in the form of bad seams and split wire.
The sheath also carries the welding current. That single fact has a practical consequence for you at the machine: the steel you are feeding is part of the circuit, and its condition — coating, rust, surface lubricant — lands in the puddle along with everything else.
The Core: Powdered Chemistry
Inside the tube sits a blend of powders, each group with a job. Mineral compounds form the slag and control its viscosity. Ferroalloys deliver deoxidizers and alloying elements in a form that dissolves cleanly in the puddle. Metal powders such as iron powder boost deposition. Gassing compounds produce the local shielding atmosphere in self-shielded grades. Arc stabilizers keep the burn even at the low currents used for out-of-position work. Binders hold the column together during manufacturing so the powder does not segregate before the tube is closed.
The formulation is matched to the intended transfer mode, position, and current range. A wire designed for flat-position high-current deposition will have a very different core than one designed to run vertically uphill at 140 amps, even though both may be sold as “flux-cored” and both may carry the same size marking on the spool.
Why the Ingredients Land on Your Side of the Equation
It is easy to treat the inside of the wire as somebody else’s department. The counterargument is in your weld logs. Arc characteristics — smoothness, directionality, spatter level — are set by the flux chemistry interacting with your voltage and stickout. Bead profile and penetration are set by the ratio of alloying and deoxidizing elements to iron powder. Slag detachability, one of the most practical day-to-day qualities of a cored wire, is set entirely by the mineral balance: too much of one oxide and the slag glues itself to the toes; get the ratio right and the slag lifts at the tap of a hammer. Corrosion resistance and low-temperature toughness come from nickel, chromium, and manganese that were metered into the blend before the wire was ever drawn.
Quick Note: Two spools with identical diameter, identical classification, and identical polarity marking can weld completely differently. The classification tells you the minimum mechanical properties the wire must meet — not how pleasant it is to run or how clean the bead looks. The formulation inside is where brands separate.
Why Raw Material Quality Decides Weld Quality
The old shop shorthand — “the wire is the wire” — is wrong in the same way that “a rod is a rod” is wrong for stick electrodes. Raw material quality in flux-cored wire shows up in three places: consistency from inch to inch, freedom from defects, and the properties of the finished weld.
Consistency: The Ingredient You Cannot See
Welding is a process that punishes variation. A flux blend that is correctly formulated on average but poorly mixed will produce a wire that behaves differently inch to inch — a foot of smooth arc followed by a foot that stutters and spatters, slag that releases on one pass and welds itself on the next. The root cause is almost always upstream: powders that were metered inaccurately, particles that segregated during storage or transport because the blend was not graded by size, or a binder that was not uniformly distributed.
Consistency begins with powder particle size distribution. Fine powders and coarse powders do not stay mixed; they migrate under vibration, which is precisely what a spool experiences in a delivery truck. Manufacturers control this by classifying powders to tight size ranges and by using binders that tack the blend together enough to resist segregation without turning it into a hard cake that will not flow through the filling equipment. When a cheap wire feeds unpredictably, you are often feeling particle segregation that happened three thousand miles away.
Purity matters the same way. Iron powder contaminated with rust or oil, fluorspar with high silica impurities, or carbonate with moisture all introduce variability — moisture in a core powder is particularly nasty because it generates hydrogen in the puddle and shows up as porosity. Our piece on flux core welding troubleshooting maps the defect symptoms that trace back to consumable problems rather than technique.
Defects That Start in the Spool
A short catalog of field defects with raw-material roots is worth keeping, because it changes where you look first when something goes wrong.
- Porosity from moisture or carbonates out of spec. Core powders that absorbed water during storage, or a formulation with more gassing compound than the wire can handle at your heat input, push gas into the puddle faster than it can escape.
- Slag entrapment from poor mineral balance. A slag that is too viscous at your travel speed gets frozen into the weld instead of floating out. This is a formulation problem more often than a technique problem.
- Unstable arc from weak stabilizer content. Low-current out-of-position work depends on ionizing elements in the flux that keep the arc path conductive. Cheap blends skimp here, and the arc wanders or extinguishes.
- Hard spots and inclusions from oversized or dirty particles. Anything in the core that does not melt and assimilate properly ends up as an inclusion — the same family of defect as porosity’s ugly cousin, and just as capable of failing an inspection.
- Cracking from alloy chemistry drift. Excess carbon, or a mismatch between deposited chemistry and the base metal, can push a weld into a hard, crack-sensitive microstructure, especially on restrained joints.
Important: Before you change settings, change liners, or change operators to chase a defect, run five inches of the same wire on clean scrap with textbook settings. If the scrap weld is bad, the problem traveled to the shop on the spool.
Properties: What the Chemistry Promises the Code
Specifications for flux-cored electrodes — the AWS A5 series documents for carbon steel, low-alloy, and stainless tubular wires — set minimum requirements for tensile strength, yield, elongation, and often impact toughness and deposited-mechanics chemistry. Meeting those numbers is a raw-material problem before it is a process problem. The nickel that gives a wire its low-temperature toughness, the manganese that contributes strength, the carbon content that must stay inside a band — all of them were decisions made when the powder bill of materials was written.
This is why reputable manufacturers publish lot certification and why builders on code work insist on it. A spool without traceable chemistry is a spool whose mechanical properties are a guess. The American Welding Society publishes these specifications through the AWS, and understanding the classification stamped on the spool — what each digit promises — is half of buying well.
Pro Tip: Keep the tag from each spool until the job is closed out. When an inspector asks what wire went into a weld, “the blue one” is not an answer; the lot number on that tag is.
The Steel Sheath: Where the Wire Starts
Between seventy and eighty-five percent of a finished spool’s weight is steel — the strip that becomes the sheath. It is the largest single raw material by mass, and it deserves more attention than it usually gets.
Strip Grade and Chemistry
Low-carbon steel is the standard choice because it welds predictably, draws cleanly, and keeps the deposited carbon content in the range the classification expects. The strip’s own chemistry feeds into the weld: the sheath melts into the puddle just like solid wire does, so its carbon, manganese, and silicon levels are part of the final weld metal analysis. A strip with wandering carbon content produces deposited chemistry that wanders with it, and the lab results that follow can put a weld outside the range the procedure qualified.
Formability and surface condition are the other requirements. The strip is folded through a series of progressive dies at speed; any inconsistency in hardness or coating shows up as inconsistent seam quality. On the drawing side, the seam weld has to survive elongation. Strip that is too brittle splits; strip that is too soft deforms unpredictably. Manufacturers specify temper and coating as tightly as they specify chemistry.
Strip Thickness and the Powder-to-Steel Ratio
The wall thickness of the finished tube sets the ratio of steel to core, which is one of the biggest behavioral differences between wire families. Gas-shielded wires typically run with a thinner flux fraction — the external gas is doing the shielding work, so the core is focused on slag, arc, and alloying. Self-shielded wires carry a heavier core because that powder has to generate the entire shielding atmosphere. The same nominal diameter can therefore hold noticeably different amounts of powder depending on what the wire is designed to do.
Diameter choice interacts here as well. Common sizes run from small-diameter wires around 0.035 inches (0.9 mm) for thin material and out-of-position work up through 1/16 inch and beyond for heavy deposition in flat positions. Smaller diameters demand finer powder blends that flow reliably through a narrower tube and meter evenly at lower fill rates. If you have ever compared two brands of the same diameter and found one visibly heavier or lighter per foot, you are looking at wall thickness and core loading decisions made by two different engineers. Our 030 versus 035 flux core wire guide covers the size decision from the operator’s side.
Coatings on the Strip
Strip arrives from the mill with its own surface condition, and manufacturers add treatments before forming. Copper coatings — familiar from solid MIG wire — appear on some cored wires to improve current transfer at the contact tip and to slow surface rust. Phosphate and other conversion coatings reduce friction through the liner and improve powder adhesion in coated constructions. Some wires ship with a light rust-preventive oil only; others go out essentially dry with an inhibitor baked into the surface treatment.
Each choice has a trade-off. Copper improves conductivity and corrosion resistance in storage but adds cost and can flake under aggressive feeding. Bare or lightly treated strip is cheaper but demands better packaging and faster consumption once opened. Nothing about this shows on the label, and it is one of the quiet differences between a spool that still welds well after three weeks in a humid shop and one that starts feeding rough after three days. Storage habits are covered in how to keep MIG wire from rusting, and the principles apply to cored spools too.
Short Note: If a cored wire arrives with rust blooms on the strip surface or white oxide on the contact tip end, the surface treatment failed somewhere in the supply chain. That is a material problem, not a feeding problem — return it while you still have the lot tag.
Ferrous Materials Inside the Core
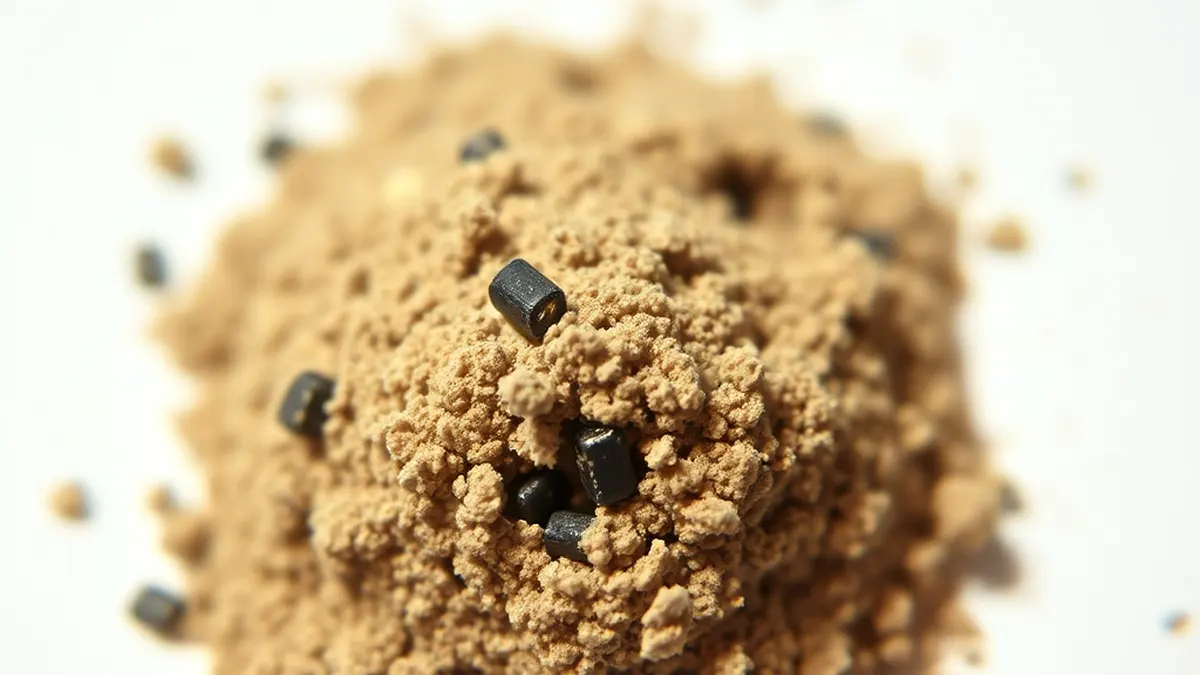
The powder column is not one substance; it is a blend of distinct materials, each with a defined role. The ferrous group — iron-bearing powders and ferroalloy particles — does the heaviest lifting in terms of mass and metallurgical effect.
Iron Powder: The Deposition Multiplier
Iron powder is the bulk filler of the core. It melts with the arc and ends up as weld metal, which means every gram of it is a gram of deposition that did not have to come through the sheath alone. This is a large part of why cored wires can deposit so much faster than solid wire of the same diameter: the core is carrying extra metal in powder form alongside the steel tube.
Iron powder also changes the electrical and thermal behavior of the puddle. More deposited metal per amp makes the process efficient, but it also means a heavily iron-loaded formulation will behave very differently at the bottom of its current range than at the top. Manufacturers calibrate iron content to the current window printed on the spool, which is one reason running a wire far below its recommended range produces a cold, ropey bead no matter how carefully you move your hand.
Quick Note: Deposition efficiency and travel speed are related but not identical. A wire with generous iron powder loading lets you move faster for the same bead size — but only if your voltage and travel speed are matched to keep the puddle fluid enough for the extra metal to wet out.
Ferroalloys: Metered Elements That Do Real Work
Ferroalloys are alloying elements packaged in an iron carrier, crushed to particle sizes that blend and melt predictably. They are how a powder blend delivers precise chemistry into a puddle that only sees the outside of a wire. The core players:
- Ferromanganese. A deoxidizer and a strength contributor. Manganese ties up oxygen that would otherwise end up as porosity or brittle oxide films, and it also scavenges nitrogen — relevant in self-shielded welding where the local atmosphere is never perfect. In the finished weld it raises strength and toughness within the limits of the specification.
- Ferrosilicon. The other workhorse deoxidizer. Silicon cleans oxygen from the puddle and helps control the shape of the bead. Too little and the weld is spongy with dissolved oxygen; too much and the deposit chemistry drifts toward an over-alloyed condition the classification will not accept.
- Ferrochrome. The basis of stainless and duplex cored wires. Chromium in the core powder is how a tubular wire can deposit corrosion-resistant chemistry without relying on a solid alloy wire of the same composition — a real advantage for stainless fabrication where flux-cored speeds beat GTAW filling rates by a wide margin.
- Ferronickel or nickel powder. Used in low-alloy grades where toughness at low temperature is the point. Nickel does not form carbides; it strengthens the matrix and keeps the weld notch-tough in cold weather, which is why impact-rated classifications carry nickel requirements.
- Ferrovanadium and microadditions. Present in small quantities in modern formulations where grain refinement or specific toughness targets justify the cost. These are the ingredients that show up in conversations about next-generation wires.
The engineering challenge is metering. Each ferroalloy has a different particle density and melting behavior; blend them carelessly and the dense particles settle during storage while the light ones float to the top of the filling hopper. That segregation is the invisible failure behind “this spool welds different than the last one of the same part number.”
Carbon Control
Carbon is the element most likely to get a weld into trouble, and in cored wire it arrives from two directions: the steel sheath itself and any carbon-bearing powder in the core, such as graphite or carbonates used for other purposes. The classification sets a ceiling on deposited carbon for good reason — beyond it, the weld metal hardens, hydrogen sensitivity rises, and the risk of cold cracking on restrained joints climbs. Managing that ceiling is a raw-material discipline: strip chemistry control on one side, powder assay and metering on the other.
If you are matching wires to joints on code work, our flux core welding polarity and settings guides cover the operator-side variables that interact with deposited chemistry — because the same wire at the wrong heat input lands in a different part of the property range than the same wire run correctly.
Non-Ferrous Raw Materials in the Core
Beyond the iron family sit the elements that give specialty wires their identity: aluminum, nickel, copper, titanium, zinc, and the occasional high-cost addition. These are used sparingly — often fractions of a percent — but their effect per gram is outsized.
Aluminum: The Scavenger
Aluminum appears in flux-cored formulations primarily as a powerful deoxidizer and nitride former. In powder form it strips oxygen from the puddle more aggressively than silicon or manganese can, and it also binds nitrogen — a useful insurance policy in self-shielded welding where the shielding envelope is generated rather than supplied from a bottle. Aluminum’s affinity for oxygen is also why aluminum-bearing wires interact with slag chemistry: the alumina that forms becomes part of the slag system rather than a gas in the metal.
For welding aluminum itself, tubular wires exist but are a different animal — the sheath and core approach is used for some aluminum-cored products, though most aluminum work still runs solid wire or GTAW filler. If aluminum is your subject, our guides on shielding gas for aluminum and flux core aluminum welding cover the process side.
Nickel and Copper: Properties and Conductivity
Nickel is the toughness workhorse of the low-alloy grades. When a wire’s classification carries a nickel designation, that nickel was metered into the core powder (or is present in the strip alloy) to deliver impact properties the plain-carbon grades cannot reach. It matters most in structural work exposed to cold — bridges, outdoor frames, equipment that will see winter — where a weld that passes a room-temperature test can still fail a notched-bar impact test at minus twenty degrees.
Copper appears in two places. Inside the core, copper-bearing powders can be used deliberately in formulations aimed at conductivity or corrosion performance. Outside, copper coatings on the sheath — covered in the previous section — are common. Because copper in a weld puddle above certain levels can cause hot cracking in susceptible alloys, its use in core chemistry is deliberate and controlled rather than casual. Solid wire’s copper coating is a frequent enough question that we wrote a whole piece on whether welding wire is copper — the short answer there and here is that coatings and core additions are engineered, not accidents.
Zinc, Titanium, and the Specialty Additions
Zinc shows up mostly in the context of coated base metals rather than as a deliberate core addition — welding galvanized sheet means vaporizing zinc that is already there, with the porosity and fume consequences that follow. Some formulations counteract zinc contamination with extra scavengers, which is a formulation-level answer to a field problem. Our piece on flux core on galvanized steel covers the technique side.
Titanium, usually as ferrotitanium, is one of the signature ingredients of self-shielded formulations. It serves as a nitrogen and oxygen scavenger and contributes to arc stability — the same element chemistry that makes rutile-bearing fluxes behave the way they do in stick electrodes. In gas-shielded grades, titanium plays a smaller role because the external gas handles atmospheric exclusion and the core is free to focus on slag behavior and alloying.
Rare earth additions appear in research formulations and marketing literature in roughly equal measure. The technical rationale — lowered work function, improved arc emission, more stable transfer at low current — is sound in principle; the practical benefit depends entirely on dose and on how uniformly those elements were distributed through the blend. Treat rare-earth claims the way you would treat any specification claim: ask for the classification, then ask for the lot certificate.
Pro Tip: Nickel is expensive. A wire priced far below competitors while claiming equivalent toughness classifications is either certified or it is not. Ask for the test report; a legitimate manufacturer will produce it without hesitation.
Flux Ingredients Explained
If ferrous powders are the body of the core, the minerals are its nervous system. This group controls the arc, forms the slag, generates the shield, and cleans the puddle — and it is where most of the formulation art lives.
Minerals and Slag Formers
Slag in flux-cored welding is not waste; it is a tool. The layer that freezes over the bead performs three jobs at once: it shields the hot metal from air while it solidifies, it holds heat in to slow cooling and improve metallurgical outcomes, and it carries impurities out of the weld as a glassy phase that lifts away when cold. The mineral ingredients that build it are chosen for melting range, viscosity, and chemical capacity.
| Ingredient family |
Typical materials |
What it does in the core |
| Fluorspar and fluorides |
Calcium fluoride |
Fluidifies the slag, widens the melting range, helps arc stability at moderate currents |
| Rutile and ilmenite |
Titanium dioxide, iron titanate |
Stabilizes the arc, builds a manageable slag, supports smooth transfer |
| Silicates and glasses |
Sodium/potassium silicates, quartz |
Viscosity control, slag structure, binder chemistry |
| Carbonates |
Limestone, calcite |
Generate carbon dioxide for local shielding — critical in self-shielded grades |
| Oxides |
Manganese oxide, iron oxide |
Slag basicity control, oxygen management, alloying contributions |
| Calcium compounds |
Calcium carbonate, wollastonite |
Desulfurizing capacity, refined slag chemistry, cleaner deposited metal |
The balance among these is what a formulation engineer actually tunes. A slag that is too fluid runs off the bead and leaves the metal exposed; one that is too stiff traps and drags. Viscosity has to suit the position too — a vertical-up wire needs a slag that solidifies quickly enough to support the puddle, while a flat-position wire can run a more fluid system that promotes puddle flow and tie-in at the toes.
Arc Stabilizers
Arc stability at the low currents used for out-of-position welding is not free — it is engineered through ionizing additives. Potassium and sodium compounds lower the ionization potential of the arc path, which keeps the column conductive and the transfer regular when the voltage and wire speed are low. Rutile contributes too, which is one reason rutile-rich formulations have a reputation for a smooth, quiet arc that beginners find forgiving.
When a wire feels “crackly” or wanders across the bead at settings where a competitor’s wire runs glassy smooth, you are usually feeling the stabilizer package. It is one of the clearest visible differences between formulations, and one of the easiest to test on scrap with both spools running the same joint.
Deoxidizers and Scavengers
The deoxidizer group — ferrosilicon, ferromanganese, aluminum, and their relatives — works in the liquid metal rather than in the slag. Their job is to tie up dissolved oxygen before it can form bubbles or brittle oxide phases as the weld solidifies. Scavengers extend the concept to nitrogen and sulfur: nitrogen forms brittle nitrides that degrade toughness, and sulfur promotes hot cracking; removing both is a chemistry race that has to finish before the puddle freezes.
This group is also why surface cleanliness and consumable condition still matter even though the wire carries its own cleaners. Deoxidizers have finite capacity. Welding over heavy mill scale or wet rust asks the core to clean more than it was designed to handle, and the excess shows up as porosity and inclusions. Prevention habits live in our flux core welding mistakes roundup.
Gassing Agents for Self-Shielded Wire
Self-shielded wire has to manufacture its own atmosphere, and it does so chemically. Carbonates decompose in the arc heat and release carbon dioxide; organic or other hydrogen-bearing components may contribute additional gas volume; titanium and aluminum compounds scavenge whatever oxygen and nitrogen slip through. The result is a local envelope that — within its design limits — keeps air away from the puddle without a bottle.
That design limit is a real one. Self-shielded wire tolerates wind far better than gas-shielded processes, but it is not immune to drafts, and the shielding volume it generates is modest compared to a proper gas envelope from a nozzle. The trade is worth understanding before a job: on a breezy site the self-shielded wire keeps working when solid wire fails, but on a precision joint with a demanding inspection regime, dual-shield wire with external gas is often the better answer. We compared the two approaches in gas MIG versus flux core and flux core versus solid wire.
Short Note: Self-shielded does not mean unshielded. The core’s generated atmosphere is engineered to a specific volume and duration — running a long arc or a very fast travel speed can outrun it just as surely as a draft blows away an argon jet.
Binders and the Making of the Wire
The powders have to become a wire, and that manufacturing sequence is itself a raw-material decision: the binder that holds the blend is part of the chemistry, and the forming and drawing steps are where weak ingredients reveal themselves.
Blending, Filling, and Forming
Production starts with assaying every incoming material — each ferroalloy lot, each mineral batch — against a specification before it enters inventory. Powders are classified by size, blended in the ratio the formulation calls for, and mixed with a binder system that keeps the blend homogeneous as it travels down the filling line. Binders are typically inorganic silicate systems or polymeric compounds chosen to burn cleanly; a binder that leaves residue changes arc behavior, so it is specified as carefully as the active ingredients.
The blend is fed continuously into a trough of steel strip that passes through forming rolls, folding the strip around the powder into a tube. A continuous resistance weld closes the seam. The filled, welded tube — still at a large diameter — is then drawn through a series of dies to the final size, with intermediate anneals as needed. Drawing compresses the core as it reduces the tube, which is why powder particle size and compressibility are manufacturing concerns and not just laboratory trivia: a blend that compresses badly can leave voids or uneven density in the finished wire.
Every step in that line can introduce defects that no operator can fix: a starved fill leaves a section of wire with less core than the formulation intends; a bad seam weld splits under drawing; a contaminated drawing lubricant works its way into the core or onto the surface. Quality control at the plant exists to catch these before the spool ships.
Spooling, Packaging, and What Happens Next
After drawing, wire is cut and spooled under controlled tension. Spooling tension matters more than people expect: a tightly wound spool deforms the wire where it crosses under the outer wraps, and those flat spots drag through the liner and arc erratically. Loose spools tangle. Packaging then has to protect the product from moisture — cored wire picks up humidity through paper and plastic if it sits long enough, and a damp core powder reintroduces hydrogen into every weld you run with it.
This is where the supply chain touches your shop directly. A wire that was perfectly made but stored in a wet warehouse is a damp wire. Ask how stock is stored, prefer suppliers who turn inventory quickly, and once a spool is open, keep it bagged. The consumable storage discipline we recommend for electrodes applies word for word to cored spools — see what is flux core welding for the fundamentals and best flux core wire for how the market’s major products are positioned.
Quick Note: The label on a cored wire spool carries the classification, the size, the recommended gas (if any), the polarity, and usually a lot number. That lot number is the link back to the assay of every powder batch that went into the spool. Keep it.
Coatings and Surface Treatments in Detail
The original strip-coating discussion in the sheath section covers the basics, but surface treatment deserves its own pass because it is the part of the raw-material spec the buyer can actually see and feel. Three properties are being engineered: corrosion resistance, abrasion resistance, and thermal stability — plus the feeding and conductivity effects already mentioned.
Protective Coatings
Corrosion protection is the first job. A bare steel sheath in a humid warehouse begins growing rust within days, and rust on the sheath means iron oxide in the puddle and inconsistent current at the contact tip. Copper plating is the most common answer — it provides a sacrificial barrier that keeps the surface bright far longer than bare steel, while also improving electrical contact at the tip. Zinc and phosphate conversion coatings are alternatives that prioritize feeding and paint-like barrier protection over conductivity. Some formulations use a thin organic lacquer instead of metal plating, trading a little current-transfer efficiency for low cost and clean feeding.
Abrasion resistance matters because the wire is dragged through liners, bends, guides, and contact tips for its entire working life. A coating that flakes under that abrasion produces debris that contaminates the liner and the tip — showing up as erratic feed and arc instability that looks like hardware failure. Thermal stability rounds out the trio: the coating must survive the heat conducted back up the wire from the arc zone without decomposing into residue that fouls the tip. Every one of these is a raw-material selection decision, and every one of them has a visible consequence in the weld.
The Function of Surface Treatments
Beyond protection, surface condition governs how the wire behaves mechanically as it travels from spool to puddle. Consistent surface finish means consistent friction through the liner, which means the drive rolls can push the wire at a steady rate without surging — the difference between a smooth arc and the intermittent stutter people blame on their machines. Good coating adhesion prevents flaking during feeding; a coating that sheds particles will plug a liner over a long day. And clean, treated surfaces improve the electrical contact at the contact tip, which stabilizes the arc voltage that your settings depend on.
None of this shows up in a classification, and almost none of it is advertised. It shows up instead in how the spool feels after a month in the shop, how often liners get changed, and whether the last foot of a partially used spool welds like the first. When you compare two manufacturers at similar price points, surface treatment is one of the quiet variables that separates them — and it is one reason a wire that feeds beautifully in your machine may feed poorly in someone else’s gun and liner combination.
Quick Note: If a wire glitters with copper dust in the liner groove and the tip keeps freezing, the coating is shedding — either a manufacturing fault or damage from storage and handling. Compare against a fresh spool before you condemn the feeder.
Formulation Families: Self-Shielded, Dual Shield, and Metal-Cored
Raw-material recipes cluster into three families, and knowing which family you are buying explains most of the behavior you will see at the machine.
Self-Shielded Wire
Self-shielded formulations carry the heaviest gassing package: carbonates, scavengers, and arc stabilizers sized to produce and maintain a local atmosphere without external gas. The trade-off shows up in the weld — the heavier flux system means more slag, somewhat lower deposited efficiency than solid wire, and a bead that is engineered for field tolerance rather than laboratory perfection. This is the wire for construction sites, outdoor repairs, and anywhere a gas line is a liability. Our gasless flux core welding walkthrough covers running it, and the Vulcan gasless experience shows what budget end of the market looks like in practice.
Dual-Shield (Gas-Shielded) Wire
Dual-shield formulations drop most of the gassing chemistry because a CO2 stream is doing that job, and reinvest the space in alloying, iron powder, and slag control. The result is higher deposition, cleaner welds, and better mechanical properties per pass — at the cost of a gas bottle and sensitivity to drafts. Most production fabrication that can protect the weld zone runs dual shield for the productivity alone. The details of the arrangement are in what is dual shield welding.
Metal-Cored Wire
Metal-cored wire is the extreme of the powder-loading approach: a thin sheath around a core that is mostly metal powder with minimal slag-forming chemistry. Deposition efficiency approaches solid wire, spatter is low, and the bead profile is wide and flat — the classic choice for high-build applications on thick plate. Because there is little slag system, the raw-material emphasis shifts almost entirely to metal powder purity and alloy accuracy rather than mineral balance. If deposition rate is your priority, compare it against solid wire directly in FCAW versus MIG.
Pro Tip: Check the label for the required shielding gas before you buy. A self-shielded spool and a dual-shield spool look alike, weld alike only in the loosest sense, and running one in the wrong configuration produces defects that look like everything except a purchasing mistake.
How Composition Changes the Weld You Get
Everything above converges on five practical outcomes: arc behavior, bead shape and penetration, positional capability, slag behavior, and final properties. The mapping from raw material to outcome is direct enough to be useful.
| Ingredient or decision |
Primary function |
What you notice at the gun |
| Iron powder loading |
Deposition filler |
Faster build-up per pass; puddle runs hotter and wetter at the same settings |
| Ferrosilicon and ferromanganese |
Deoxidation, alloying |
Cleaner puddle, fewer gas defects, strength contributions in test coupons |
| Nickel additions |
Toughness |
No visible effect — it shows up in impact test results on qualified procedures |
| Rutile and silicates |
Arc stability, slag structure |
Smooth, quiet arc; predictable slag release |
| Carbonates and gassing agents |
Local shielding |
Tolerance of light drafts on self-shielded grades; porosity if overwhelmed |
| Fluorspar content |
Slag fluidity |
How easily the slag lifts and how well the toes wet out |
| Strip surface treatment |
Feeding and conductivity |
Consistent current at the tip, less liner friction, storage life |
Penetration and Bead Shape
Alloy and mineral balance influence heat distribution as surely as your voltage dial does. Formulations tuned for deep penetration on butt joints run differently from those tuned for bridging gaps on poor-fit-up field work — the latter typically carry more iron powder and a slag system that tolerates a wider, shallower puddle. This is why “same class, different brand, different bead” is so common: the classification fixes the mechanical floor, not the profile.
Travel speed interacts here too. A wire designed for high-speed flat work will look anemic at slow hand speeds, and a wire designed for careful out-of-position runs will underperform when someone opens the feed and tries to make up schedule. Match wire family to joint geometry first, then set parameters. Our amperage chart and 116-series settings guide give the machine-side ranges for common configurations.
Positional Capability
Vertical and overhead welding demand a puddle that freezes fast enough to support itself while still wetting the edges — a narrow window that is largely set by the flux formulation. Arc stabilizers keep the transfer regular at the low currents needed for position work; slag that sets quickly holds the metal up; iron powder loading is kept moderate so the puddle does not become too fluid. This is the chemistry behind the common experience of a wire that runs beautifully flat and fights you uphill: the formulation may simply not be built for the position, no matter what the label’s classification technically permits.
Technique still matters enormously once the formulation is right — push angle, stickout, weave width. We collected those habits in flux cored arc welding techniques and the position-specific walkthroughs like vertical up settings.
Slag and Cleanup
Slag detachability is the most user-visible quality in a cored wire and the most direct readout of mineral balance. A well-formulated slag peels in complete ribbons as the bead cools; a poorly formulated one sticks at the toes, demands grinding, and hides whatever it is sitting on. Shop foremen learn their crews’ preferred wires partly on this criterion alone, and they are not being sentimental — a wire whose slag lifts clean saves real minutes per foot on a long job.
Short Note: When slag suddenly starts sticking on a wire that used to peel, suspect moisture or storage before you suspect the manufacturer. Damp flux changes viscosity. Bag the spool, dry the environment, and run a test bead before you reject the formulation.
Feeding and Electrical Behavior
The sheath’s surface treatment and the wire’s dimensional consistency govern feeding. Coated wires slide through liners more uniformly; wires drawn to tight diameter tolerance keep the contact tip engagement consistent, which keeps the arc consistent. Rough or out-of-round wire shows up as erratic current, tip burn-back, and the kind of stutter that gets misdiagnosed as a drive-roll problem — sometimes correctly, which is why checking rolls and liners against wire condition is standard practice. We covered the hardware side in drive rolls for flux core wire.
Raw Materials, Fume, and Shop Safety
There is a less obvious consequence of core chemistry: what comes out of the arc as fume. Welding fume composition follows the consumable and the base metal — a stainless cored wire carries chromium and nickel in its fume, a galvanized job carries zinc, and flux ingredients themselves contribute to the particulate mix. Fluoride-bearing flux chemistry, common in formulations built for slag fluidity, is one more reason extraction at the source is not optional on enclosed work.
The regulatory framework runs through constituent limits rather than a single fume number, with manganese, iron oxide, and hexavalent chromium among the measured species; NIOSH treats welding fume as carcinogenic and recommends keeping exposure as low as feasible. The controls are the ones any experienced welder already knows: a fume extractor positioned close to the arc, respirators only within a written program, and material choices made with the exposure in mind. Read the source material at OSHA’s welding page, and see our own are welding fumes toxic and respirator guide for the practical side.
Important: Low-fume formulations exist and are a legitimate purchasing criterion on enclosed or repetitive work. The fume generation rate is a direct function of what is in the core — a raw-material decision with a direct occupational-health consequence.
How Raw Materials Get Verified
Reputable manufacturers treat incoming materials as controlled inputs, because the cost of a bad batch discovered in production — or worse, discovered by a customer — dwarfs the cost of testing.
Assay and Incoming Inspection
Every ferroalloy and mineral lot is sampled and assayed before it is released to the blending line. Chemistry is checked against specification; particle size distribution is verified because blending and flow behavior depend on it; moisture content is measured on hygroscopic materials. Suppliers are qualified and re-qualified, and certificates of analysis travel with each lot. NIST’s work on measurement standards and reference materials underpins exactly this kind of industrial chemistry — traceable measurement is what makes a specification more than a wish.
In-Process and Final Checks
On the line, checks cover fill density, seam integrity, diameter tolerance, and surface condition. Finished wire is verified against the classification it claims: mechanical testing of deposited weld metal, chemistry of the deposit, and — where the specification calls for it — impact and bend testing. Manufacturers then confirm behavioral qualities that no certificate fully captures, like slag release and arc smoothness, through trial welds. When a manufacturer publishes a performance claim alongside a classification, the classification is the auditable part.
On your side of the transaction, the equivalent practice is simple: buy from suppliers who can produce lot documentation, keep the tag, and run a trial bead whenever a new lot enters rotation. Technical background on consumable testing and procedure qualification is well covered by TWI’s knowledge resources, and manufacturers such as Lincoln Electric publish the specification sheets that tell you which AWS document governs a given spool. Testing a spool on scrap costs minutes; discovering chemistry drift in the middle of a pressure-tested assembly costs weeks.
Quick Note: Lot traceability cuts both ways. If a weld ever fails analysis, the tag tells everyone which raw-material lots were involved — which protects you as much as it protects the manufacturer.
Sustainability: Recycled Materials and Responsible Sourcing
Flux-cored wire sits inside one of the most recycled material streams on earth. Steel strip is predominantly made from recycled scrap, particularly in electric-arc-furnace production, and that reality shapes the environmental profile of every spool sold.
Scrap Utilization and Landfill Reduction
Using recycled metal as the feedstock for sheath steel dramatically reduces the reliance on virgin ore extraction, and the same logic applies inside the core: iron powder is frequently produced from reclaimed or byproduct streams, and some manufacturers deliberately specify recycled content where purity permits. Every kilogram that comes from a scrap stream is a kilogram that never came out of a mine and never went to a landfill. The environmental arithmetic of metals recycling is well documented — the EPA’s materials pages summarize the benefits of recycling and sustainable materials management for anyone who wants the broader picture.
Energy and Lifecycle
Recycled steel requires significantly less energy than primary production from ore, which is why the steel industry’s recycling rate is a point of pride and why sourcing decisions ripple outward. Lifecycle assessment — evaluating a material from extraction through manufacture, use, and disposal — is increasingly part of how large buyers choose suppliers, and wire makers respond with documentation of energy use and emissions per ton. The Department of Energy publishes context on industrial energy use and efficiency that explains why this matters at scale.
Sourcing Discipline
Beyond recycled content, responsible sourcing covers mineral procurement — fluorspar, rutile, and specialty ores are mined somewhere, under someone’s labor and environmental standards. The practical version of this for a welding buyer is unglamorous but effective: prefer manufacturers who can describe their supply chain, who package efficiently, and who turn stock quickly so that product is not destroyed by warehouse damp before it is ever used. Wire that rusts in storage wastes every resource that went into making it.
Short Note: The greenest spool is the one that welds well and gets consumed. Buying the cheapest wire available and scrapping half of it because of defects is not thrift — it is paying twice with interest.
Future Trends in Wire Raw Materials
The formulation side of this industry moves slowly — welding metallurgy is conservative for good reasons — but three directions are worth watching.
Advanced and Microalloying Additions
Microalloying — additions measured in parts per million rather than percent — lets manufacturers refine grain structure and improve toughness without changing the classification. Grain-refining additions produce finer as-welded structures, which translate directly into impact performance and fatigue resistance. Some of the same concepts travel from research into commercial blends faster than others; the test is always whether the wire still behaves predictably at the bottom of its current range, because exotic chemistry that only works in a narrow window does not survive contact with fabrication shops.
Refined Flux Formulations
Particle-size engineering and purer mineral grades are lowering spatter and improving slag detachability across the market. Better-classified powders segregate less, blend more uniformly, and feed more consistently — improvements that show up as “this new spool just runs nicer” without any change in the operator. Expect continued tightening of powder specifications rather than dramatic new ingredients.
Greener Chemistry and Manufacturing
Two pressures are converging: fume reduction and environmental compliance. Formulations that generate less particulate per kilogram deposited, binders with lower decomposition products, and manufacturing processes with smaller energy footprints all fit the direction travel regulations are taking. For the welder, the benefit is practical — less extraction required for the same work, and consumables that stay usable longer in storage.
Pro Tip: Treat ingredient innovation claims the way you would treat a horsepower claim on a lawnmower. Ask what classification the wire meets, what lot testing supports it, and how it runs at your settings on your metal. Marketing is not a certificate of analysis.
How to Judge a Spool at the Counter
Most readers will never spec a powder blend, but everyone can apply a buyer’s checklist. This is the distilled version of everything above, in the order it pays to apply it.
- Start with the classification, not the price. The AWS class stamped on the spool — and the specification it references — sets the mechanical floor. If a bargain wire cannot produce documentation for the class it claims, walk away.
- Match the family to the job. Self-shielded for field and wind, dual shield for production and properties, metal-cored for deposition. Buying the wrong family guarantees a bad experience regardless of quality.
- Confirm the size against your hardware. Drive rolls, liner, and contact tip must match the diameter, and the wire’s recommended current range must overlap the machine’s output on the position you plan to run.
- Look at the spool itself. Even winding, no rust on the visible strip, intact packaging, a legible label with a lot number. Rust and damage at the counter do not improve in your shop.
- Ask about storage and turnover. A supplier with fast inventory movement is selling you fresher flux than one clearing old stock. Moisture-sensitive product has a shelf life in practice even when it has none on paper.
- Run a qualification bead. Clean scrap, textbook settings, the joint you actually intend to weld. Judge arc smoothness, slag release, bead profile, and the absence of porosity. Five minutes of evidence beats an hour of reviews.
- Keep the tag. Lot number filed with the job paperwork turns a future problem into a traceable event instead of an argument.
Quick Note: Consistency across spools is the mark of a real manufacturer. Buy two spools of a new wire at once and run both early — if they behave differently, you have found out cheaply what a large job would have taught you expensively.
Frequently Asked Questions
What is flux-cored wire used for?
Structural steel fabrication, pressure and pipe work within the relevant specifications, shipbuilding, heavy equipment repair, outdoor construction, and any job where deposition rate, positional capability, or tolerance of imperfect field conditions matters. The tubular construction lets a single consumable cover a wider range of thicknesses and positions than most solid-wire setups.
What materials make up flux-cored wire?
A low-carbon steel strip formed into the sheath, plus a core of iron powder, ferroalloys such as ferromanganese and ferrosilicon, minerals like rutile and fluorspar, arc stabilizers, gassing compounds in self-shielded grades, and a binder that holds the blend together during manufacture. Specialty grades add nickel, chromium, or titanium-bearing compounds for toughness, corrosion resistance, and arc performance.
How does flux-cored wire improve welding?
The core carries shielding chemistry, deoxidizers, alloying elements, and extra filler metal directly into the puddle. The practical results are higher deposition per amp, better out-of-position capability, tolerance of less-than-perfect surface condition compared with solid wire, and slag coverage that protects the bead as it freezes. Those advantages are all direct consequences of the raw materials described above. Background on the process itself is in what is flux core welding.
Can flux-cored wire be used outdoors?
Yes — self-shielded grades were designed for exactly that, and they tolerate wind far better than gas-shielded processes. “Tolerant” is not “immune”: strong drafts still overwhelm the generated atmosphere, and every formulation has a limit. For windy sites the alternative comparison is in gas versus flux core.
Why does the same classification weld differently across brands?
Because the classification specifies outcomes, not recipes. Iron powder loading, slag system, stabilizer package, particle engineering, and surface treatment all vary between manufacturers while still meeting the same mechanical minimums. The formulation is where a brand’s engineering shows.
Does flux-cored wire go bad on the shelf?
The steel does not expire, but the flux can absorb moisture and the surface can corrode if packaging is breached. Store spools sealed, off the floor, and dry; if the core powder has taken on moisture you will see porosity and hear it in the arc. Storage guidance for the parallel case of stick electrodes is in drying welding rods.
Conclusion
Every spool of flux-cored wire is a bundle of engineering decisions disguised as a commodity: the grade and coating of the steel strip, the purity and particle size of the iron powder, the metering of ferroalloys that set your weld’s chemistry, the mineral balance that decides whether the slag lifts clean, and the gassing package that keeps air out of the puddle. The wire that feeds smoothly, peels slag in ribbons, and passes inspection is not lucky — its raw materials were specified, tested, and blended by somebody who knew what the weld would demand.
For the person buying and running that wire, three habits cover most of the ground. Read the classification and get documentation for it. Match the formulation family to the environment — self-shielded for the field, dual shield for controlled production, metal-cored for build-up. And verify on scrap before production, because five minutes of test welding tells you more about a spool’s chemistry than any label ever will.
Treat the consumable as part of the procedure rather than an incidental purchase, and the defect conversations that used to eat shop time — the porosity, the sticking slag, the stuttering arc — get shorter, because you will know which of them start at the powder blend instead of at the machine. When you want to go deeper on the process side, our guides to troubleshooting and weld strength pick up where the raw materials leave off.