When Was TIG Welding Invented? The True History of GTAW (1941 and Beyond)
When was TIG welding invented? Russell Meredith perfected Heliarc (GTAW) in 1941. Learn the full history, patents, evolution…
READ ARTICLE →The shop I learned TIG in had a scarred gray cabinet with one drawer nobody labeled. Inside were loose tungsten electrodes of every color, tossed together like mismatched sockets: green, gray, blue, red, gold, a few brown ones nobody could explain. One Saturday a customer dropped off a pair of 6061 motorcycle brackets that needed invisible seams, and the old timer on second shift handed me a green tungsten, shrugged, and said, “For aluminum, this one.” The arc started, it wandered two inches across the joint, it popped, and the tungsten tip took a bite of the puddle. I re-ground it, tried again, got maybe an inch of decent bead before the arc nose-dived into the plate. Only then did the old timer wander over, swap in a gray electrode, cut the amperage by twenty, and show me what a stable AC arc actually looks like: a tight hissing cone, a clean etched band either side of the puddle, and a bead that stepped like a row of stacked dimes. That ten-minute lesson stuck harder than anything I read in a manual. The color stamped or tipped on your tungsten is not decoration; it tells you what oxide is blended into the tungsten, which tells you how the arc will start, how long the tip will last, and whether the electrode survives alternating current at low amps. For welding aluminum on AC TIG, green (pure) and gray (ceriated) tungsten are the classic choices, blue 2% lanthanated and gold 1.5% lanthanated are the versatile modern picks that run on both AC and DC, brown 0.4% zirconiated is an AC specialist, and red 2% thoriated is a DC electrode you should generally keep away from aluminum. That is the short answer, and the rest of this guide explains why each color behaves the way it does, what diameter to run, how to prep the tip, and how to pick the right electrode for the thickness and amps sitting in front of you.
Before we go further, a quick word about how we will treat colors here. Manufacturers do not all mark tungsten the same way, and the tip color you see in a package does not always match the AWS classification printed on the box. One brand’s green is another brand’s plain unalloyed rod. The reliable way to know what you are holding is the classification code stamped on the electrode itself, and we will decode that shortly. Keep the color as a shortcut and the classification as the truth.
Aluminum is a stubborn metal to arc, and the tungsten sits right at the point where physics, chemistry, and operator feel collide. Three properties of aluminum make electrode selection matter more than it does on mild steel. First, the oxide skin. Bare aluminum melts around 1,220 degrees Fahrenheit, but the aluminum oxide sitting on top of it does not melt until roughly 3,700 degrees Fahrenheit. That is a threefold gap, and it is the single reason TIG on aluminum uses alternating current: the positive half-cycle blasts the oxide off, the negative half-cycle drives heat into the work. Second, thermal conductivity. A 1/8 inch aluminum plate pulls heat away from the weld zone several times faster than the same thickness of mild steel, so your arc has to be consistent and focused or the puddle simply refuses to wet out. Third, fillers are sensitive. 4043 and 4047 rods melt at far lower temperatures than the base metal, which means the arc has to preheat the joint evenly without wandering onto the filler and turning it into a basketball.
The tungsten electrode is what holds all of that together. It is the non-consumable element in the process, so everything about its alloy, diameter, and tip geometry shapes how the arc behaves during both halves of the AC cycle. A soft arc from pure tungsten will spread heat gently and forgive sloppy technique. A pointed, alloyed electrode will focus that heat into a narrow cone that lets you stack a 1/16 inch fillet on 0.063 sheet without burning through. Neither is universally right. Choosing badly does not always produce a failure you notice immediately; sometimes it produces a weld that looks acceptable and has buried lack of fusion because the arc was never actually stable.
Think about what happens sixty times a second when your machine is set to AC. During the electrode-positive portion, ions slam into the tungsten tip and heat it hard. During the electrode-negative portion, electrons pour out of the tip and into the work. Pure tungsten handles that back-and-forth by forming a rounded ball at the tip, which is exactly what you want for a soft, wide arc across a cleaning-heavy joint. Alloyed tungstens like ceriated or lanthanated resist that balling and hold a point instead, which gives a tighter arc but asks more of the tip’s metallurgy. If you run a pointed alloyed electrode at very high AC amperage without enough ball or without enough mass, the tip spits and deforms. If you run a pure electrode at low AC amperage, the ball will not form reliably and the arc wanders. Matching the electrode to the current and the amps is the entire game.
Welders talk about arc stability as if it were an abstract spec. It is not. A stable AC arc on aluminum sounds like a hard, even hiss with a faint crackle, and the cleaned etch zone stays symmetrical on both sides of the bead. An unstable arc sounds intermittent and spitty, the arc cone flickers wide and narrow, the etch band comes out lopsided, and the tungsten tip visibly glows and dims with the pulse of the current. If you have ever chased a puddle that kept freezing on one side of the joint while the other side went molten, you were probably fighting an electrode that could not hold focus at your amperage. Electrode choice is the first variable to change before you touch machine settings, and it is the cheapest fix on the cart.
Quick Note: Arc instability on aluminum is usually blamed on dirty metal or bad gas coverage, and those are real culprits. But after the joint is acetone-cleaned and your cup is flowing correctly, the tungsten is the next suspect. Swap the electrode before you rebuild the whole setup.
The American Welding Society publishes the specification that governs tungsten electrodes for arc welding, AWS A5.12. Inside that document each alloy gets an EW designation built from the alloying element: EWG for pure or generic tungsten, EWCe for ceriated, EWLa for lanthanated, EWZr for zirconiated, EWTh for thoriated, EWW for tungsten heavy metal alloy, and so on. Those codes are stamped or laser-etched on most electrodes in 7-inch or 7-10 inch lengths, and they are far more trustworthy than the color of a painted tip because colors are not standardized across manufacturers.
| Tip Color | AWS Designation | Alloy Blend | Typical Current | Fit for Aluminum AC |
|---|---|---|---|---|
| Green | EWG | Pure tungsten, 99.5%+ | AC preferred | Yes, classic choice |
| Gray | EWCe-2 | 2% cerium oxide | AC / DC | Yes, strong at low amps |
| Blue | EWLa-2 | 2% lanthanum oxide | AC / DC | Yes, all-purpose |
| Gold | EWLa-1.5 | 1.5% lanthanum oxide | AC / DC | Yes, all-purpose |
| Brown | EWZr-0.4 or EWZr-1 | 0.4% to 1% zirconium oxide | AC only | Yes, AC specialist |
| Red | EWTh-2 | 2% thorium oxide | DC preferred | Not recommended |
| Violet | EWY | Yttriated (rare) | AC / DC | Situational |
The pattern is simple once you see it. EW means electrode tungsten. The letters that follow name the oxide additive, and the number is the percentage of that oxide in tenths or whole percent depending on the brand. A rod marked EWG is straight tungsten with no meaningful alloy, which is what most people mean when they say green. EWCe-2 carries two percent cerium. EWLa-2 carries two percent lanthanum. If a rod carries no marking at all, assume it is generic pure tungsten and treat it like green until proven otherwise. When you buy in bulk boxes, the classification is printed on the label; when you scavenge from that unlabeled shop drawer, drag a file across a corner and read the stamp.
Colors on tungsten originally followed a convention, but the convention drifted once aftermarket manufacturers entered the market. The most common source of confusion is ceriated tungsten: some brands tip it gray, others tip it orange, and a few use a light blue that people mistake for lanthanated. Lanthanated 2% is nearly always blue, but a couple of European packs label it differently. Thoriated is reliably red, and zirconiated is reliably brown, so those two are safe to trust. The lesson is practical: memorize the AWS code first and let the color be a secondary hint. A $12 magnifying glass and a spare minute at the bench will save you an afternoon of chasing an arc you do not understand.
Short Note: Some manufacturers color-code both ends of the electrode and print the classification between the marks. If the print has been ground off during use, the tip color is all you have left, so mark your keeper tubes with a paint pen the moment you open a new box.
Green tungsten, technically EWG, is unalloyed tungsten with a purity around 99.5 percent or higher. It has been the default aluminum electrode for decades because of how it behaves under alternating current: it forms a smooth, rounded ball at the tip, and that ball throws a soft, forgiving arc. On a shop machine running 120 to 180 amps on 1/8 inch aluminum, green tungsten gives you a wide, gentle heat pattern that blends nicely and tolerates a slightly out-of-position torch angle. For students and hobbyists it remains a perfectly reasonable electrode, and it is usually the cheapest rod in the display case.
The softness that makes green forgiving also makes it imprecise. The ball grows as you weld, the arc cone widens with it, and at low amperage the ball never forms properly, which is where the wandering starts. Pure tungsten also erodes faster than alloyed types under AC because the ball tips spatter slightly with each polarity flip. Expect to re-grind green tungsten more often, and expect the tip diameter to drift through the day unless you stop and reshape it.
If your work is mostly 1/8 inch-and-up aluminum brackets, frames, and repairs, green tungsten will serve you for years. If you bought your TIG machine to weld soda-can-thin material or to run beautiful food-grade seams on stainless pipe as well, you will outgrow green in a weekend.
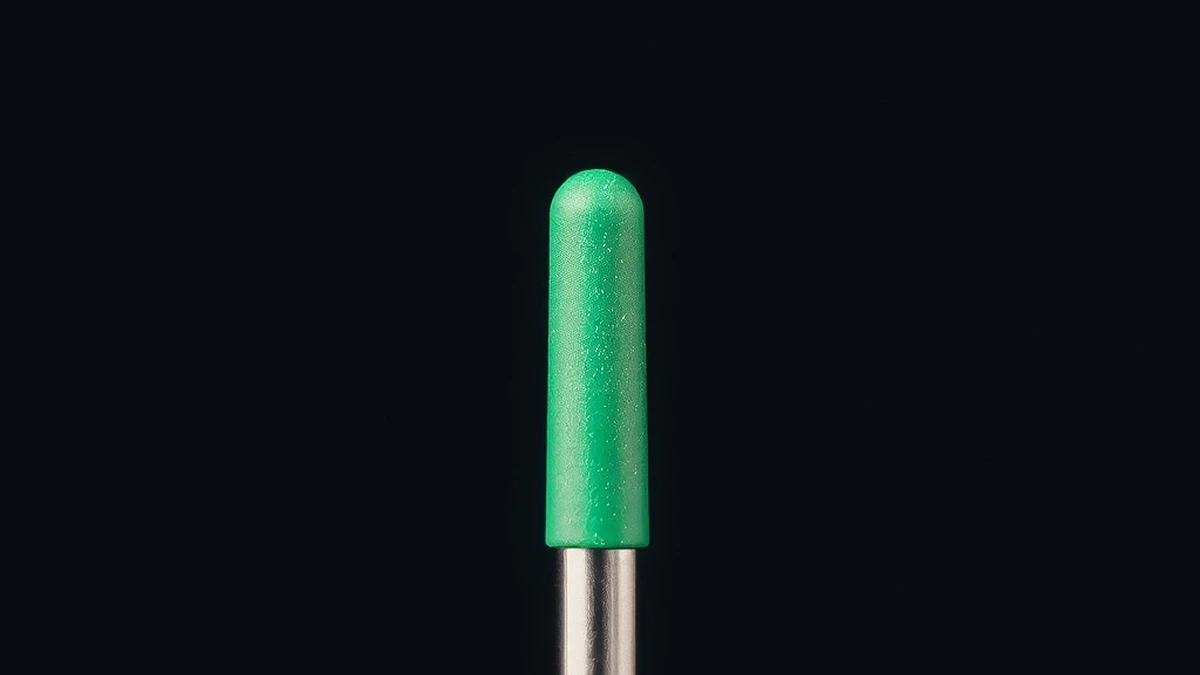
Ceriated tungsten, marked EWCe-2 and usually tipped gray, blends about two percent cerium oxide into the tungsten matrix. Cerium lowers the work function of the electrode, which is a fancy way of saying electrons leave the tip more easily, so the arc starts at lower voltage and holds together when the current drops. On aluminum that translates into a point that stays a point under AC, a crisp arc cone, and noticeably less tip erosion than pure tungsten at the same amperage. For anyone welding thin aluminum, this is the electrode that feels like an upgrade the first time you strike an arc.
Ceriated performs beautifully on DC as well, which makes it a genuinely dual-purpose rod if you weld steel and stainless with the same set of tungstens. The trade-offs are modest: ceriated costs more per rod than pure tungsten, and at very high AC amperage the pointed tip can erode more aggressively than a balled pure electrode because there is no ball to absorb the ion bombardment. Shops running sustained 250-amp AC work should note that limitation before standardizing on gray.
The sweet spot for ceriated sits roughly between 40 and 150 amps on AC. In that window the arc starts on the first try without scratching, the cone stays narrow enough to focus heat on a 1/16 inch fillet, and the etch band comes out even and controlled. Welders doing aluminum throttle bodies, small enclosures, bicycle frames, and electronics chassis tend to standardize on gray for exactly this reason. One shop I worked with ran 0.063 sheet all day, and their crews burned through roughly one gray tungsten per shift against two or three greens for the same output, purely because re-grinding stops disappeared.
| Factor | Green (EWG) | Gray (EWCe-2) |
|---|---|---|
| Approximate price per 10-pack | Lower | Moderate |
| Re-grinds per shift (typical) | More frequent | Less frequent |
| Stability at 60 amps AC | Poor | Excellent |
| Stability at 250 amps AC | Good (balled) | Fair to good |
| Works on DC for steel too | Poor | Excellent |
| Best suited user | Thick aluminum, students | Thin aluminum, precision, mixed metals |
Look at the hidden costs and gray usually wins inside a month. Every re-grind costs a minute of labor, a burst of shielding gas, and a chance to contaminate the tip with fingerprints. Multiply by a crew of four and the price gap between the two electrodes disappears. Pro Tip: If you buy tungsten in bulk, price it per amp-hour of welding rather than per pack. A cheaper rod that forces twice the re-grinds is the expensive rod.
Lanthanated tungsten came onto shop floors as the electrode that wanted to do everything. Blending lanthanum oxide into tungsten produces a rod that starts easily, holds a point under AC, resists erosion on DC, and keeps arc stability across a wide current range. In practice that means one box of blue tungsten can cover your aluminum AC work, your mild steel DC work, and your stainless work without swapping electrodes when the job changes. For a small shop or a home garage with limited drawer space, that versatility is the whole argument.
There are two common lanthanated recipes, and they are more similar than different. The two percent version is almost always tipped blue; the one-and-a-half percent version is tipped gold. Both conduct well, both tolerate AC and DC, and both run cooler at the tip than thoriated at equivalent amps on DC. The practical difference shows up at the extremes: blue tends to hold up slightly better at high current, gold behaves marginally better at the very bottom of the amperage range. For 90 percent of aluminum work you could flip a coin.
Blue EWLa-2 is the electrode most often recommended when a welder asks for one rod to cover everything. It handles AC balancing on aluminum without balling on many machines, starts reliably from a cold tip, and runs 30 to 40 amps higher in continuous service than ceriated before erosion becomes a problem. On a machine with a modern inverter AC wave, blue holds a tight cone even when you drop to 40 amps for tack work, which is exactly where pure tungsten falls apart. If you weld aluminum one day and fabrication steel the next, blue is the pragmatic choice. You can see the same logic in equipment reviews like our picks for the best TIG welders built for aluminum work, where machines are judged on how cleanly they hold low-amp AC for thin material.
Gold EWLa-1.5 is the quieter sibling. It draws slightly less current to initiate the arc, which makes it a favorite for inverter machines with high-frequency starts and for welders who do a lot of tacking where the arc has to fire dozens of times per part. It is also forgiving if you accidentally run it on DCEN for a quick steel tack after finishing an aluminum run, which happens constantly in mixed-fabrication shops. Some welders report that gold produces a marginally quieter arc and a slightly smoother bead profile on thin aluminum; others cannot tell the difference in a blind test. What everyone agrees on is that gold and blue are both safely above pure ceriated or pure tungsten for versatility.
Important: Lanthanated tungsten does not need to be balled on most inverter AC machines, and forcing a heavy ball on it will soften the arc and defeat the point of the alloy. Follow your machine manufacturer’s electrode prep instructions, which are usually printed in the TIG section of the manual.
Zirconiated tungsten, EWZr, is tipped brown and exists almost entirely for alternating current on aluminum. The zirconium oxide content (commonly 0.4 percent, sometimes 1 percent) gives the electrode excellent resistance to the contamination that AC imposes on the tip, and it holds a slightly rounded end that spreads the arc in a way aluminum likes. Historically it was the electrode of choice on old transformer AC machines before inverter technology made low-amp AC easier, and it still shows up on aluminum-heavy production lines running transformer or simple square-wave power sources.
The limitation is straightforward: zirconiated is an AC rod. Run it on DCEN for steel and it will erode quickly and spit. For a welder who only touches aluminum, brown is a legitimate option, but for anyone with a mixed workload it is one more box in the drawer for a job the blue lanthanated already covers. The zirconiated arc is also a touch softer than lanthanated at the same settings, which helps on thick plate and hurts on thin sheet. If you are setting up a dedicated aluminum welding station for heavier sections, brown deserves consideration; otherwise the all-purpose rods win on convenience.
Red tungsten, EWTh-2, contains about two percent thorium oxide and has been an industry workhorse for generations. On DCEN welding of steel, stainless, and titanium, thoriated electrodes deliver superb arc starts, strong current-carrying capacity, and long service life. Those same properties do not transfer to AC aluminum work. Under the electrode-positive half of the AC cycle, thoriated tips overheat and erode unevenly; the point rounds, spits, and can shed small particles into the puddle. Arc starts become erratic, and the tungsten tends to crack or split at the tip after repeated AC cycles.
There is also a safety dimension that pure tungsten and lanthanated do not share. Thorium is a weakly radioactive element, and grinding thoriated tungsten produces a fine dust that should not be inhaled or scattered across the shop. NIOSH has studied welding fume exposure for decades and its guidance on respiratory protection applies directly here, and OSHA’s welding, cutting, and brazing standard sets the baseline for ventilation and housekeeping in any shop that grinds electrodes. None of this makes thoriated dangerous to use in a normal welding operation, but it does mean extra handling discipline for a rod that offers no benefit on aluminum AC in the first place.
Those habits line up with the general practice described in OSHA’s welding and cutting overview and with the exposure guidance published by NIOSH’s welding program. A solid shop safety routine covers electrode grinding too.
Thoriated is not obsolete. For DCEN welding of carbon steel, stainless, and most nonferrous work on DC, red tungsten starts fast, carries heavy current, and lasts. Many pipe shops standardize on it for their DC work and simply keep a separate box of blue or gray for the aluminum machine. If your shop welds aluminum strictly on one dedicated TIG unit and steel on another, split the stock: red on the DC rig, lanthanated or ceriated on the AC rig. That separation also eliminates the accidental cross-contamination problem where a rod used on steel gets dropped into an aluminum job. Our comparison of tungsten versus stainless steel electrodes goes deeper on that distinction.
Aluminum welding is an AC process for one reason: cleaning action. During electrode-positive time, argon ions scrub the oxide layer off the joint; during electrode-negative time, heat flows into the base metal to melt it. The ratio between those two phases is your balance setting, and it directly changes what your tungsten endures. More cleaning (higher EP percentage) heats the tip harder and erodes pointed electrodes faster. More penetration (higher EN percentage) cools the tip but risks leaving oxide in the puddle. Electrode selection and balance settings have to be tuned together, which is why a rod that behaves perfectly at 70 percent EN can misbehave at 50 percent EN.
| Scenario | Suggested Current | Suggested Tungsten | Balance / Notes |
|---|---|---|---|
| Thin aluminum, 0.050 to 0.090 in | AC, 40 to 90 A | Gray ceriated, gold lanthanated | Lean toward penetration; pointed tip |
| General 1/8 in fabrication | AC, 90 to 160 A | Blue lanthanated, green pure | Even balance, 65 to 75% EN on inverters |
| Heavy plate 1/4 in and up | AC, 180 to 320 A | Green balled, blue lanthanated | More cleaning; watch tip erosion |
| Cast aluminum repair | AC, variable | Blue lanthanated, brown zirconiated | Dirty casting needs cleaning time |
| Steel and stainless on same machine | DCEN, as required | Red thoriated, blue lanthanated | Never run aluminum rods cold on DCEN without checking |
Older transformer machines expressed balance as percent cleaning, newer inverters usually express it as percent electrode negative. Watch the manual, because 70 on one machine can mean the opposite of 70 on the other. A practical starting point for clean aluminum is 70 percent EN (which equals roughly 30 percent cleaning) on an inverter. Push cleaning higher when the casting is old and contaminated, but back off if your tungsten tip starts glowing cherry and deforming within seconds of arc start. If the etch band shrinks and the puddle refuses to wet, you are cleaning too little. This kind of dialing-in is exactly what our aluminum TIG settings chart walks through for common thicknesses, and our broader TIG settings reference covers amperage-per-thickness rules for other metals.
There are legitimate cases for welding aluminum on DCEN. Some aluminum alloys, notably certain copper-bearing 2xxx series aerospace alloys, are welded on DCEN with helium or helium-argon mixes because AC cleaning can damage the metallurgy or because penetration profile matters more. Thin aluminum tube work sometimes uses DCEN with a helium-rich gas to keep heat input low and travel fast. These are specialized processes, and the electrode choices narrow to ceriated or lanthanated because they tolerate DCEN without the erosion problems thoriated shows on AC. If you are not doing aerospace or specialty tube work, assume AC and move on. For a broader look at the current question, our guide on TIG welding aluminum on DC explains when it works and when it does not.
Short Note: Helium mixes run hotter than pure argon, which changes tungsten heat load completely. If you switch shielding gas mid-job, re-evaluate your electrode diameter before you re-evaluate your technique.
Color gets you the right alloy; diameter gets you the right arc. An electrode that is too small for the current will overheat, ball up uncontrollably, and contaminate the puddle. One that is too large will refuse to start reliably, wander at low amps, and force you to crank heat you did not want. The classic guideline for AC TIG on aluminum runs roughly 1 amp per 0.001 inch of diameter for pure tungsten, with alloyed pointed electrodes able to run slightly hotter for their size because the point concentrates current differently. Use these ranges as a starting bracket and adjust for your machine’s actual behavior.
| Tungsten Diameter | Recommended AC Amperage | Common Aluminum Thickness | Best Alloy Choices |
|---|---|---|---|
| 1/16 in (1.6 mm) | 30 to 90 A | 0.040 to 0.125 in | Gray, gold, blue |
| 3/32 in (2.4 mm) | 80 to 200 A | 0.090 to 0.250 in | All colors; the shop default |
| 1/8 in (3.2 mm) | 150 to 300 A | 0.190 to 0.500 in | Green balled, blue, brown |
| 5/32 in (4.0 mm) | 220 to 400 A | 0.375 in and heavier | Blue, green, brown |
| 3/16 in (4.8 mm) | 330 to 550 A | Heavy plate, molds | Blue, green, large cast |
The 3/32 inch rod is the answer to most first-time questions because it spans the widest useful band. Keep a bundle of 1/16 for thin work and a bundle of 1/8 for heavy, and you have covered nearly everything a general shop sees. Buying advice on electrode sizing and machine pairing is collected in our guide to TIG electrodes for aluminum and our roundup of the best tungsten options for aluminum.
Pro Tip: Hold the torch like you are welding, then look at how much tungsten sticks past the gas cup. Roughly 1/8 inch of stick-out for a 3/32 rod is a good starting point. Too much stick-out starves the puddle of gas; too little puts the cup in your line of sight and invites contamination.
Two prep philosophies exist for aluminum TIG, and picking the wrong one for your alloy will undo everything you did right with color selection. Pure tungsten gets balled. Alloyed tungstens get ground to a point. There are edge cases, particularly zirconiated on AC and lanthanated on some inverter waves, where a very slight radius is preferred over a needle point, but the broad rule holds.
To ball green tungsten for AC, strike an arc on a scrap aluminum block at moderate current and let the tip melt back into a rounded dome. The ball diameter should be roughly 1.5 to 2 times the electrode diameter, no larger. Excessively large balls wander, and a ball that is too small defeats the purpose. Once formed, keep the current at or below the level that created the ball; push the amperage higher and the ball will grow mid-weld and change your arc profile halfway through a seam. Balling is a lost skill on modern inverter machines because many of them run pointed electrodes on AC without issue, but if you are running a transformer or a scratch-start rig, balling is still the correct prep.
Alloyed electrodes must be ground lengthwise, with the grind marks running parallel to the axis of the rod, not around the circumference. Circumferential grinding creates micro-channels that give the arc a path to spin around, which shows up as a wandering or rotating arc cone. Use a dedicated tungsten grinder or a fine diamond wheel, keep the included angle between 20 and 30 degrees for general work (narrower for low-amp precision, wider for high current), and grind only the exposed tip, never the body where your classification mark lives. Contamination is the other killer: never touch the ground tip with bare fingers, and never lay a freshly ground electrode on a dirty bench. Oils from skin bake onto the tip at arc temperature and seed the very contamination you are trying to avoid, and electrode contamination is addressed in the same housekeeping framework as OSHA’s respiratory protection and cleaning requirements for welding operations.
Quick Note: If your tungsten keeps getting contaminated on the start rather than during the run, the problem is almost always technique or gas coverage, not alloy. Lower the high-frequency start current, slow your approach, and check that the gas post-flow is actually protecting the hot tip after you release the trigger.
Abstract advice only goes so far, so here is how the color question played out in three real situations I have hands-on familiarity with. Each shop made a defensible choice, and each choice tells you something about how to think about your own drawer of tungsten.
Scenario one: the motorcycle bracket shop. A four-person operation welding 0.090 and 0.125 inch 6061 brackets, roughly forty parts a day, all AC TIG on inverter machines. They started with green tungsten because it was cheap and the owners had always used it. Rework hovered around 8 percent, mostly porosity and a few cold starts that left a crater at the tie-in. They switched the crews to 3/32 ceriated gray and kept the green only for the heavy jig tables. Within a month rework dropped to about 3 percent, and the crews stopped complaining about arc crawl on the short tacks where amperage dipped under 70 amps. The gray rod cost maybe twenty dollars more per month across four machines. The rework they avoided was worth ten times that.
Scenario two: the one-man restoration garage. This welder restores old aluminum fuel tanks, trim, and cast housings, and his work jumps from 0.040 sheet to half-inch cast in the same afternoon. He standardized on 2% blue lanthanated in three diameters: 1/16 for sheet and trim, 3/32 for general work, 1/8 for the heavy cast sections. One alloy across the board meant he never had to think about which rod was in the machine, and his spare parts bill for tungsten dropped to nearly nothing because lanthanated rods lasted through weeks of mixed use. When he does DC steel repair on the same machine, he does not swap electrodes at all; blue handles it. His argument for the setup is simple: fewer decisions, fewer mistakes, and our guide to the best aluminum welders for beginners makes the same point about simplifying your first rig.
Scenario three: the trailer fabrication line. Bigger shop, heavier work: 1/4 inch and 3/8 inch plate joints, long seams, high daily arc time. Transformer machines with a ball-prep bench. Green pure tungsten at 1/8 and 5/32 diameter, balled each morning, is the standard here because at 250 to 350 amps the ball is stable, the arc is soft enough to blend the joint, and green rods are cheaper per foot of weld on sustained high-current duty. Lanthanated would work too, but the shop foreman has decades of ball-prep habit and the machines are not inverters. The lesson cuts both ways: the “best” tungsten is the one matched to the machine, the amperage, and the operator’s workflow, not the one with the newest marketing.
Quick Note: If you are setting up a new station, decide your alloy before you buy diameters. Buying three sizes of the wrong alloy is the most common and most expensive tungsten mistake in small shops.
Arc stability is not a vanity metric; it shows up in the finished weld as specific, diagnosable defects. When the arc cone flickers or wanders, heat input stops being constant, and the puddle responds by alternately freezing and flooding. On aluminum that reads as a bead with inconsistent width, ripples that vary in spacing, and an etch zone that is wide on one side of the seam and narrow on the other. Lack of fusion follows, because the arc spent part of its time pointed somewhere other than the root. On thin material you get burn-throughs that seem to appear out of nowhere, usually right where the arc jumped.
Contamination is the other stability casualty. A wandering arc tends to dip toward the puddle, and once tungsten touches molten aluminum the electrode is contaminated and must be re-ground. Re-grounding mid-job costs time and, more importantly, invites the habit of grinding with whatever wheel is nearest, which can deposit steel particles onto the tungsten. From that point forward the arc will not run clean no matter how good the alloy is.
A quick scenario makes this concrete: a welder on a hydraulic repair job kept getting what he called “spider tracks” along otherwise decent beads on 1/4 inch aluminum box tube. He had cleaned the metal twice and replaced his gas line. What he had not noticed was that his 3/32 pure tungsten had been balled at 130 amps and he was welding at 240, so the ball was melting wider every few inches and shifting the arc. Moving to a 1/8 balled green rod at the same current cured it immediately. The electrode was wrong for the amps, not the technique or the gas.
Important: Diagnose in this order: metal cleanliness, gas coverage, machine settings, then electrode. Electrode is cheapest to test but it is not always first. Swapping tungsten on a dirty joint just hides the real problem for another hour.
Most tungsten problems come from a handful of repeat errors. Here is the pattern recognition list that saves the most time on a busy bench.
Each of these shows up in the training material produced by industry bodies such as the American Welding Society, which publishes the electrode specifications and the performance standards the whole trade leans on.
Electrode selection does not happen in isolation. Shielding gas, filler alloy, and cup geometry all push on the same arc, and a mismatch between them will make a good tungsten look bad.
Gas. Nearly all aluminum TIG runs on 100 percent argon, and that is the right default. Argon gives a softer arc that is easy to control at low amps and provides the cleaning action AC needs. Helium or argon-helium blends run hotter and travel faster on thick stock, but they also increase tungsten heat load, so you may need to step up electrode diameter or move to an alloy that tolerates the extra heat. For standard work, argon at 15 to 20 cubic feet per hour with a properly sized cup is the baseline. Our breakdown of the right gas for aluminum welding covers flow rates and cup pairings in detail, and the common mistake of reaching for a mixed gas is addressed in our explainer on 75/25 argon-CO2 on aluminum. Short version: CO2 is not your friend here.
Filler. 4043 is the forgiving general-purpose rod for non-heat-treated alloys and castings; 4047 flows wider and lower; 5356 is stronger and harder but more prone to cracking if the technique is sloppy. Filler choice affects how much heat your arc needs to maintain the puddle, which indirectly affects how hard the tungsten works. A puddle that is starved because the filler keeps stealing heat will make you raise amps, which can push an electrode past its comfortable range. Our roundup of the filler rods used for aluminum work gives the alloy-by-alloy detail.
Cup size. A number 5 cup focuses gas tightly for small, low-amp work where a 1/16 rod is doing the job; a number 12 or a gas lens feeds a broader, calmer column for high-amp seams. If your arc looks fine until you lengthen stick-out, the cup is the problem, not the electrode. A good starting setup for mixed aluminum work: 3/32 lanthanated, number 8 cup, 18 to 20 CFH argon, roughly 1/8 inch stick-out. Adjust from there based on what the puddle tells you. For a wider look at process selection before you commit to TIG, our side-by-side of MIG, TIG, and stick explains where each process wins.
Pro Tip: When troubleshooting an arc problem, change only one variable at a time. Swap the tungsten first, then gas, then cup. Change three things at once and you learn nothing about what fixed it.
The tungsten market has not stood still. Lanthanated electrodes were the first major shift away from thoriated dominance, driven by the desire to avoid radioactive material handling altogether without giving up arc performance. More recently, yttriated and mixed-oxide electrodes have appeared, marketing better arc focus and longer life on AC inverter machines. Some carry violet or white tip codes and are priced at a premium. Independent testing generally shows they perform at least as well as lanthanated on aluminum, with the biggest gains in arc start consistency rather than raw life. Whether that justifies the price depends on how much you weld.
The larger trend is machine-driven. Modern inverter power sources with adjustable AC waveforms, pulse capability, and high-frequency starts are far more forgiving of electrode choice than the transformer machines of the past, and they reward pointed alloyed tungsten at low currents where old machines demanded a ball. As those inverters have taken over shop floors, sales of pure green tungsten have declined while lanthanated and ceriated have climbed. Our coverage of the best-value aluminum TIG machines reflects that shift: nearly every current recommendation is an inverter with AC pulse, precisely because it unlocks low-amp work that used to require very specific electrode handling.
Industry standards evolve alongside the hardware. Electrode classifications and testing requirements live in documents maintained by organizations like the American Welding Society, and any change to classification affects what ends up on the shelf at your supply house. Keeping a loose eye on those revisions is not exciting, but it does explain why a box of tungsten bought five years ago might carry a slightly different marking than the replacement you ordered last week.
Short Note: Newer blends are rarely a downgrade, but they are also rarely a revolution for hobbyist work. If blue lanthanated is already serving you well, a violet premium rod will not transform your beads. Save experiment money for gas, filler, and a better cup first.
Tungsten electrodes are small, expensive, easy to drop, and surprisingly easy to ruin. A storage and handling routine sounds like overkill until you watch a bag of mixed rods hit the floor and then get swept into a corner. The fix is boring and effective: keep each alloy in its own labeled tube, keep tubes in a drawer divided by alloy, and never loose-mix colors again after the incident that started this article.
Welding itself produces fume, and the fume from base metal and fillers deserves respect regardless of which tungsten you run. NIOSH has published extensively on welding exposure, and its guidance is the most practical starting point for any shop writing a ventilation plan; NIOSH’s welding topic page collects the current recommendations. Thoriated tungsten adds a small additional consideration at the grinding stage. The controls are unglamorous: exhaust at the source, a respirator when engineering controls cannot capture the dust, and wet wiping instead of dry sweeping. Pair those with general hot-work practices and you cover the realistic risks. A broader reference for what OSHA expects from any welding operation is the agency’s welding and cutting safety page.
Quick Note: If your shop shares space with an office or a clean assembly area, grinding dust travels. Grind near the exhaust, not near the open door to the office, and everyone downstream of you will quietly thank you.
If the alloy tables feel like a lot, collapse the decision into four project categories. Match the job in front of you to the row, and you will be right the overwhelming majority of the time.
| Project Type | Typical Thickness | Recommended Tungsten | Diameter | Tip Prep |
|---|---|---|---|---|
| Soda-can-thin sheet, electronics, model work | 0.020 to 0.063 in | Gray ceriated or gold lanthanated | 1/16 in | Sharp point, fine grind |
| General shop fabrication, brackets, frames | 0.090 to 0.190 in | Blue lanthanated (green acceptable) | 3/32 in | Point on inverter, ball on transformer |
| Heavy plate, structural, trailer work | 0.250 in and up | Green pure or blue lanthanated | 1/8 to 5/32 in | Ball on AC, moderate point |
| Cast aluminum repair, dirty castings | Varies | Brown zirconiated or blue lanthanated | 3/32 to 1/8 in | Slight point, tolerate contamination |
| DC steel and stainless on same machine | Varies | Blue lanthanated or red thoriated | 3/32 to 1/8 in | Sharp point, longitudinal grind |
For someone building a first kit without overspending, buy three tubes and stop worrying: 3/32 blue lanthanated as the workhorse, 1/16 gray ceriated for thin material and low-amp tacks, and 1/8 green pure for heavy AC work if you own a transformer machine. That trio covers essentially every aluminum job a home welder encounters, plus DC work on steel, and it costs less than a decent filler rod order. Add a fine diamond hand file or a small dedicated grinder, a tube for cut-offs, and a marker, and your tungsten program is complete. If you are still choosing the machine itself, our guide to the cheapest aluminum welding routes compares where to spend first, and our beginner welding tips cover the habits that make any electrode work better.
Pro Tip: Buy one more box of your workhorse diameter than you think you need. Running out of the right tungsten mid-job is how people end up welding aluminum with a rod that was never suited to it.
The same handful of questions come up whenever tungsten colors come up. Here are direct answers, no hedging.
There is no universal winner, but if forced to name one rod for a modern inverter machine doing typical aluminum work, 2% blue lanthanated in 3/32 is the safest single answer because it handles AC and DC, starts reliably, and tolerates a wide amperage range. If your machine is an older transformer and your work is thicker, green pure with a balled tip remains entirely valid. If your work is mostly thin sheet at low amps, gray ceriated will feel better than anything else in the drawer.
You can strike an arc with it, but it is a poor fit for AC aluminum and is not recommended for routine use. Thoriated tips erode and spit under the electrode-positive half-cycle, arc starts become erratic, and the rod offers no benefit on aluminum that lanthanated or ceriated do not already provide. It also brings radioactive-material handling considerations that pure or lanthanated rods avoid entirely. Keep red for DC work.
Only if you are running pure green tungsten on an AC machine that expects a ball, typically a transformer or scratch-start unit. Alloyed electrodes like ceriated, lanthanated, and zirconiated are usually run pointed or with a very slight radius on modern inverters, and forcing a heavy ball on them softens the arc and wastes the alloy’s advantages. Check your machine manual; it will state the expected prep for AC.
Splitting is almost always thermal or prep related. The electrode was run above its current capacity, balled too large and then overheated, or it was a pure rod pointed to a needle so the tip could not dissipate heat. Contamination and repeated rapid thermal cycling from long post-flow gaps contribute too. Fix it by stepping up diameter, reducing amperage, correcting tip geometry, and confirming gas post-flow is cooling the tip gradually instead of shock-quenching it.
3/32 inch is the correct diameter for that range, and it is also the range where almost any alloy behaves well. Blue lanthanated or gray ceriated at a point on an inverter, green pure balled on a transformer. Going up to 1/8 inch at 150 amps is possible but the arc will feel less focused and starts will be fussier; going down to 1/16 will overheat the tip.
Not meaningfully. Gas flow is driven by cup size, stick-out, draft conditions, and amperage, not by electrode alloy. Where alloy can matter indirectly is if a poor choice forces you into a wider arc and more cleaning, but that is a settings issue. Set flow for the cup and the environment: roughly 15 to 20 CFH through a standard number 8 cup in still air, more in a drafty bay. Our dedicated piece on shielding gas choices for aluminum covers that in depth.
For occasional mixed work, yes: blue lanthanated handles AC aluminum and DC steel without a swap. For dedicated production where each machine runs one process, splitting stock is more efficient and prevents contamination mistakes. If you run flux core or MIG alongside TIG, the gas and wire choices change completely, which our comparison of flux core versus MIG explains.
Premium rods are usually consistent rather than magically better: tighter diameter tolerance, cleaner alloy distribution, and more reliable classification marking. On a precision low-amp job that consistency shows up as fewer bad starts. On rough fabrication you will not notice. Buy from a supplier with fast turnover so the stock is fresh, and judge brands by how they behave over a full box, not by the first rod.
Strip away the tables and the alloy chemistry and the decision reduces to a few moves you can make this week.
Do that and the color on the end of your tungsten stops being a mystery and starts being a tool. The arc will start cleaner, the tip will last longer, and the beads will stack more predictably, whether you are tucking a seam on 0.040 sheet or running a long joint through quarter-inch plate. If you want to go further on the surrounding skills, our walkthroughs of practical TIG techniques, TIG strength compared with MIG, and aluminum-ready TIG machines build naturally on what you have read here. Pick one change from the list above, apply it on your next job, and let the bead tell you whether you chose right.