MIG Pak 10: Specs, Settings, Duty Cycle & Real-World Guide
MIG Pak 10 guide: real specs, duty cycle, polarity for flux-core vs gas, settings chart, troubleshooting, safety, and…
READ ARTICLE →A shop we work with runs two identical Ironman 240s on their fabrication floor. One of them has been welding structural frames five days a week for years. The other sits on a cart next to a plasma table and mostly runs sheet. Neither has been kind to it: the sheet-metal machine gets dragged across concrete, plugged into whatever outlet is free, and asked to run light wire all morning. Both still strike an arc on the first trigger pull.
That is the whole review in one sentence, but it is not the whole review, because the interesting questions are elsewhere. What does 280 amps actually buy you over a 200-amp machine? What is the catch on a 186-pound welder? Why does the spec sheet say 60 percent duty cycle when nobody ever welds at exactly 200 amps? And is the jump from the Ironman 230 to the 240 a real engineering change or a model-number change?
This Hobart Ironman 240 review answers those questions with the numbers from Hobart’s own spec sheet, the details that matter on a shop floor, and an honest list of who should not buy it.
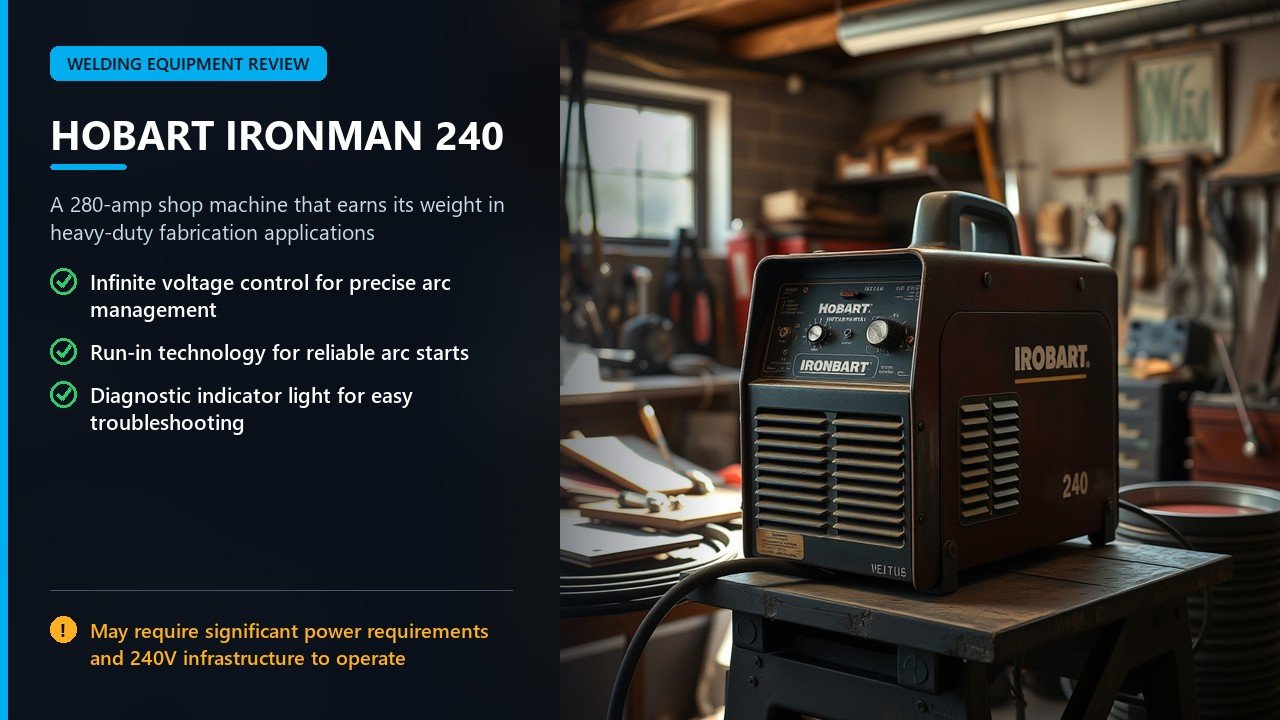
Short answer: The Hobart Ironman 240 (model 500574) is a 240V, transformer-based MIG and flux-core welder with 30–280 amps of output, rated 200 A at 60% duty cycle, welding 24-gauge to 1/2-inch mild steel in a single pass. It adds infinite voltage control, run-in arc-start technology, and a diagnostic light to the Ironman 230 platform — real upgrades, not cosmetics. It is built for fabrication shops, farms, and serious garages with 240V power; at 186 pounds and MIG-only, it is neither portable nor multi-process. At around $2,200 it competes with machines costing more, and its 5/3/1 warranty is among the best in its class.
| Specification | Hobart Ironman 240 |
|---|---|
| Model number | 500574 |
| Processes | MIG (GMAW) and flux-cored (FCAW) |
| Input voltage | 208/240V single-phase (listed 220/230/240V) |
| Amperage range | 30–280 A |
| Rated output | 200 A at 24 VDC, 60% duty cycle |
| Duty cycle at higher output | About 32% at 240 A; 100% around 160 A |
| Open circuit voltage | 40 VDC |
| Wire feed speed | 50–700 ipm, infinite control |
| Voltage control | Infinite (not tapped) |
| Mild steel thickness | 24 ga to 1/2 in. (13 mm), single pass |
| Input at rated load | 11.4 kVA / 7.1 kW (about 50 A at 240 V) |
| Weight | 186 lb. (84 kg) |
| Dimensions (H×W×D) | 30 × 19 × 40 in. |
| Spool capacity | 4- and 8-inch spools (2, 10, 33, 45 lb.) |
| Spool gun | SpoolRunner 200 ready (sold separately) |
| Warranty | 5/3/1-year limited |
| Typical price | Approximately $2,000–$2,300 |
One number in that table deserves attention before anything else: the machine pulls roughly 50 amps of input current at rated output on a 240-volt circuit. That is not a plug-and-wall-outlet welder. Planning the electrical service is half the purchase decision, and we will come back to it.
The Ironman 240 sits in an awkward and honest spot: too much machine for a hobbyist who occasionally welds, exactly right for someone who welds daily and has the power and space to support it.
The package is complete, which sounds like faint praise until you buy a competitor’s machine and discover the regulator is an accessory. Out of the carton you get:
What is not in the box: shielding gas, wire (beyond what you buy separately), and any form of PPE. Standard for the category, worth stating because the machine welds the moment you connect the essentials.
Setup is genuinely fifteen minutes if you have done it before and thirty if you have not. Connect the work cable, screw the gas hose to the regulator, thread wire through the drive system, set liner and contact tip, set the chart’s suggested voltage and wire speed for your material, and strike an arc. Nothing in the process is proprietary or fiddly.
The machine announces its intentions physically. At 186 pounds and 30 inches tall on a wheeled cart with a cylinder rack, it is imposing next to a 110-volt handler — and deliberately so. The frame is steel, the panels are steel, and the drive system housing is aluminum rather than the plastic you find on entry-level machines. The hinged front door opens to reveal the settings chart positioned directly below the two control knobs, which is exactly where your eyes are when you are adjusting. Whoever laid out that panel had spent time setting up machines.
The controls are two knobs: voltage and wire feed speed. Infinite on both. There is no display, no menu, no synergic mode that picks settings for you — and for this class of machine that is a feature rather than a gap. A transformer machine with infinite controls gives you an arc you tune by ear and eye, which is how fabricators actually work. Machines with digital interfaces do not weld better; they guess faster. Whether you want the guessing is a preference question, and the 240 takes a clear position on it.
The wheels deserve mention because cheap carts ruin good machines. The running gear is industrial — the kind that survives a concrete floor and the occasional dropped cylinder — and the cylinder rack carries a standard size bottle without a bungee ritual. Roll it to the work, set the bottle brake, and weld.
Feature lists on welders are mostly noise. These are the ones that change how the machine behaves.
The Ironman 230 gave you twelve voltage taps. The 240 gives you a continuous range from minimum to maximum, and this is the single most consequential upgrade for anyone welding anything thinner than structural plate. Tapped machines force you to pick the closest of twelve positions; the arc you get is the arc that exists. Infinite control lets you split the difference — settle the puddle on 18-gauge by dialing a hair off the tap you would have been stuck with, or add exactly enough heat to get flat profile on 3/8-inch without going one step too far.
Wire feed gets the same treatment: 50 to 700 inches per minute with no detents. Combined with the chart inside the door, you set a proven starting point and then adjust in the direction the puddle tells you to, rather than in the jumps a tapped machine forces. If you have learned on a twelve-position machine, the first hour with infinite control feels like switching from a staircase to a ramp.
Arc starts are where beginners burn wire and where experienced welders judge a machine. When you pull the trigger on most wire feeders, the wire arrives at full programmed speed before the arc exists — the wire stabs the plate, bounces, and spatters until the arc catches up. Hobart’s run-in feature slows the wire to a preset creep until arc initiation, then ramps to your set speed. The result is a start with dramatically less spatter and no bird’s-nest of wire where you were aiming.
This matters more than it sounds. A third of the spatter complaints in any shop trace back to starts, not to travel. It also protects thin material: a wire striking 24-gauge at full feed speed is a punch, not a start. The feature existed on the 230’s more expensive relatives and its absence on older machines was a common complaint — its arrival on the 240 closed a real gap.
One light, three signals: steady means the machine is thermally overloaded and needs to cool; a double blink means a wire-feed problem, usually a jam or a stick; a triple blink points at the drive system or gun. It is not a digital display and does not pretend to be. What it does is end the era of staring at a silent machine trying to remember whether the last time it did this it was hot or fed-up.
Thermal overload protection itself is the important part: when you genuinely exceed the duty cycle — and you will, on a long seam — the machine shuts down cleanly instead of cooking its transformer. The light tells you it is thermal rather than broken, which saves a service call that would have been a coffee break.
The wire drive is a dual-geared system in an aluminum housing — geared, not the single-idler plastic setups on entry machines. Geared drive means both drive rolls grip with equal pressure, which is what keeps feed speed consistent when you are pushing wire through 15 feet of liner against the resistance of a spool brake set correctly. Aluminum housing rather than plastic means the drive system does not flex under load, and flex is what turns into feed inconsistency on long runs.
Feed consistency sounds like a spec-sheet virtue until you weld a two-foot fillet at one speed setting and watch the bead width breathe. Consistent penetration needs consistent wire delivery; consistent delivery is a mechanical property of the drive, not an electronic feature. This is the kind of component that decides whether the machine still welds the same in year five.
The spool hub takes 4- and 8-inch spools — the 2-, 10-, 33-, and 45-pound rolls the industry actually ships. A 45-pound spool is what a production shop runs; a 10-pound roll is what a farm keeps for repair; being able to use either without an adapter is basic competence that not every machine offers. The brake tension knob releases the spool for a change in seconds, and the hinged feeder panel opens wide enough that you are not threading wire through a slot.
Below the knobs, a click-open compartment holds contact tips, nozzles, and the drive roll you are not using. It is a small thing that saves the ten minutes per job of walking to the parts cabinet because your spare tip walked off.
The fan runs when the machine needs cooling and stays off when it does not. Two benefits: the shop is quieter during setup and between passes, and — more importantly — an always-running fan pulls shop dust, grinding grit, and metal fines into the machine’s internals all day. A fan that runs on demand contaminates the machine far less, which is a longevity argument more than a comfort one. It also means the noise of the machine tells you something: when the fan cuts in on a hot day, you are approaching the duty-cycle boundary.
Related, from our duty cycle guide: keeping intake paths clear and the machine out of direct sun does not raise the rating, but it stops you from derating yourself through neglect.
The headline number — 60 percent duty cycle — is true and slightly misleading, in that order. It is measured at rated output, which for this machine is 200 amps, over a ten-minute window: six minutes welding, four minutes off. It is not the duty cycle at every setting.
The actual curve, from the machine’s own duty cycle chart, looks more like this:
| Output | Approximate duty cycle | What it looks like in practice |
|---|---|---|
| 160 A | 100% | All-day welding on light-to-medium work with no pauses |
| 200 A | 60% | Six minutes on, four off — the rated condition |
| 240 A | About 32% | Thirds: weld a third of the time on heavier work |
| 280 A | Below 20% | Burst output for the hardest passes, then cool-down |
The useful way to read that: this is a machine that welds continuously at 160 amps and nearly continuously at the heat most MIG work actually runs. Two hundred amps of short-circuit and globular transfer covers the overwhelming majority of fabrication. The 280-amp ceiling exists for the times you need spray transfer on thick material or you are pushing hard; nobody runs a full day at maximum output on any transformer machine in this class, and the ones that claim otherwise are measuring differently.
Practically, if your work lives under 200 amps — and unless you weld plate all day, it does — you will almost never wait for this machine. If you do hit the limit, the diagnostic light tells you why instead of leaving you to guess.
Specifications describe what a machine can be asked to do. Arc quality is what it actually does when you ask. On the Ironman 240, three things stand out.
With run-in engaged, the wire meets the work gently and the arc catches without the pop-and-sputter ritual. On a fresh nozzle and correct stick-out, starts are repeatable: trigger, brief pause as the wire creeps, arc, and you are running. On thin material this is the difference between starting a weld and blowing a hole you have to fill. Used machines from this lineage earn reputations for starting well for exactly this reason — the feature is mechanical in effect and does not degrade the way an electronic soft-start on a cheaper machine can.
The arc is characterized by good wetting — the puddle spreads into the joint rather than sitting on top of it — with light spatter when settings are right. That last clause does real work: infinite controls make it easy to be right. On short-circuit transfer at normal fabrication settings, spatter is low enough that post-weld cleanup is a brush rather than a chipping session. When you are wrong about settings, the machine gives you a clear visual signal in the bead, which is how you learn to correct it; machines with soft, forgiving arcs that hide bad settings teach you nothing.
Half-inch in a single pass is the published capability on mild steel, and while single-pass thick welds always benefit from joint preparation, the machine has the thermal headroom to make good on it. More relevant is the bottom of the range: 24-gauge capability with 30 amps of minimum output means the same machine that welds frame rail also runs sheet, provided you set it correctly and use the right wire. The gap between a machine’s floor and its ceiling is what makes it a shop machine rather than a project machine.
One performance note from the spec sheet, easy to miss: open circuit voltage is 40 VDC. Higher OCV makes arc starting easier and more reliable, particularly with larger diameter wire and on cold days. It is also in the range where standard PPE discipline applies — the arc will find your eyes if you let it, which is true of every welding machine ever made and worth repeating in any review that a beginner might read.
The 230 was a respected machine with a cult following. The 240 replaced it with real changes, and the comparison table is where you can see which ones matter to you:
| Feature | Ironman 230 | Ironman 240 |
|---|---|---|
| Amperage range | 30–250 A | 30–280 A |
| Rated output | 200 A at 60% (rated at 175 A) | 200 A at 60% duty cycle |
| Voltage settings | 12 tapped positions | Infinite |
| Wire feed | Up to 700 ipm | 50–700 ipm, infinite |
| Open circuit voltage | 38 VDC | 40 VDC |
| Run-in technology | No | Yes |
| Diagnostic indicator | No | Yes |
| Spool gun ready | Yes | Yes |
| Duty cycle at 200 A | 60% at 175 A | 60% at 200 A |
Reading it honestly: the welding core is an evolution, not a revolution. The 230 already laid a good bead, and owners who loved its arc character had no reason to doubt the 240 would keep it. What the 240 genuinely adds is control resolution (infinite instead of twelve taps), arc-start refinement (run-in), and self-diagnosis (the indicator light), plus 30 more amps at the top.
The voltage story is the one to be careful about. Some write-ups describe the 240 as having “12 taps with better fine control” — that describes neither machine; the 240’s control is continuous, and that is the point. If you are deciding between a used 230 and a new 240, the honest framing is: the 230 welds well and the 240 welds well with more room to tune. The decision should be made on price, condition, and warranty, not on the expectation of a different puddle.
Two processes, three materials, one qualifier each.
Solid wire with shielding gas for anything you want to weld and not grind, gasless flux-core for outdoor and dirty-material work. The machine runs both polarities — check our MIG polarity explained guide if you have ever flipped a switch and gotten porosity instead of an answer. Steel from 24-gauge to half-inch covers automotive work, trailers, frames, guards, gates, and most general fabrication. This is what the machine was built to do, and it does it without qualification.
Supported with tri-mix gas and stainless wire, with the usual caveats that apply to every MIG-welded stainless: heat input control matters more than on mild steel, and the infinite voltage control helps here more than on almost any other application. If you weld stainless regularly as a primary material rather than an occasional one, dedicated machines and TIG will always outperform MIG on appearance — but for brackets, fixtures, and food-truck fabrication, this machine is capable.
The Ironman 240 is spool gun ready. Spool gun ready means the machine has the control connection and drive capability for the SpoolRunner 200 — a 20-foot cable with a 4-inch spool on the gun itself, rated 200 amps at 60 percent, welding 16-gauge to half-inch aluminum with .030–.035 wire. No adapter box, no external control board: plug the power pin into the feedhead, attach the trigger lead, and go. You do need to buy the spool gun separately, and it is not inexpensive — but the machine-side support being built in rather than bolted on is the correct way to do it.
Why a spool gun at all: aluminum wire is too soft to push reliably through a 15-foot liner — it buckles, jams, and birds-nests. The spool gun puts the wire supply inches from the contact tip, which is the entire reason the accessory exists. Anyone who has tried to run aluminum through a standard gun and blamed their technique has really been fighting physics. For a deeper look at the options, our best MIG welders for aluminum and can you weld aluminum with a MIG welder guides cover the trade-offs.
No stick. No TIG. No aluminum without the optional gun, and no aluminum through a standard MIG gun regardless of what you have read. If your work mixes processes — say, stick for outdoor pipe and MIG for shop fabrication — this machine covers half of it, and you will be carrying a second machine. That is a legitimate reason to choose a multi-process unit instead, with all the trade-offs that entails.
The Ironman 240 draws approximately 11.4 kVA — around 50 amps of input current at 240 volts at rated load. That has consequences, and they are the kind that are cheap to plan for and expensive to discover.
The honest summary: budget for the electrician alongside the welder. A $2,200 machine on a $300 circuit problem is a $2,500 problem with two site visits in it.
One hundred and eighty-six pounds, thirty inches tall, forty inches deep including the cart and cylinder rack. This machine occupies floor space the way a piece of shop equipment should: visibly, permanently, and with the cylinder hanging where a cylinder belongs rather than chained to a wall.
The wheels make it rollable around a shop floor with one hand, which is what matters day to day — the machine goes to the workpiece, not the reverse. Transporting it between sites is a different question: 186 pounds needs a ramp or two people and a truck, and the machine should be secured upright with the cylinder removed. Shops that move welders regularly typically allocate one machine to stay put and one to travel; trying to make a single 186-pound machine do both means one of the two jobs is done badly.
The footprint also includes honest clearance: ventilation intake paths need room, the front door needs room to swing for the chart, and the gun lead needs room to reach. On a crowded bench, plan the position before the first weld, not after the third untangle.
Against its class, the Ironman 240 is unusually friendly — and the reason is not the manual, it is the chart.
Inside the hinged door, the weld, set-up, and parts information chart gives starting voltage and wire speed for material type and thickness. The knobs are directly above it. You read the chart, set the knobs, weld a test bead, and adjust from a known-good starting point rather than from a guess. For someone who has set up machines before, this is fifteen minutes of work. For someone who has not, it is the difference between a first weld and a first disaster.
Operationally, the machine has exactly two adjustments and a gas flow. That is the entire interface. There is no synergic wizard, no menu tree, no pulse mode to misconfigure. You set heat and speed, you control the rest with your hands, and the machine does not second-guess you. Beginners adapt to this quickly because there is nothing to adapt to — and experienced welders prefer it because a machine that guesses is a machine arguing with you.
The genuine limitation for newcomers is not usability but economics: learning puddle control on 24-gauge in a machine with this much headroom means you are using a fraction of what you paid for. If your trajectory is “hobby now, production later,” buying forward makes sense. If it is “hobby indefinitely,” the Handler line is the same company’s answer at a fraction of the weight and price.
The chart inside the door is the authority, but having realistic starting numbers in your head before you open it saves a test plate. The following ranges are sensible first positions for common jobs on this machine — set here, run a bead, then adjust voltage and wire feed together in small steps based on what the puddle tells you. Our full MIG wire speed and voltage chart goes deeper if you want the reasoning behind each column.
| Material | Wire | Gas | Voltage | Wire feed |
|---|---|---|---|---|
| 24–22 ga steel | .023–.030 solid | 75/25 C25 | Low-mid range | Slow — creep, do not chase |
| 18–16 ga steel | .030 solid | 75/25 C25 | Mid range | Moderate; watch for burn-through |
| 1/4 in. steel, fillet | .030–.035 solid | 75/25 C25 | Mid-high range | Match to voltage; flat profile target |
| 3/8–1/2 in. steel | .035 solid | 75/25 C25 (or C100 for spray) | High | High — this is where 240+ amps live |
| Outdoor or dirty steel | .030–.035 flux-core | None (self-shielded) | Typically one step hotter than solid wire | Check polarity — FCAW runs DCEP |
| Stainless steel | .030 stainless | Tri-mix (90He/7.5Ar/2.5CO2) | Conservative — heat input shows | Moderate |
| Aluminum (with SpoolRunner) | .030–.035 aluminum | 100% argon | Mid-high; aluminum wants heat | Confident — do not starve the puddle |
Three habits make the chart work for you rather than instead of you. First, always test on a scrap piece of the same material and thickness you are about to weld — offcuts from the actual job beat any table ever printed. Second, change one variable at a time; when you adjust voltage and wire feed simultaneously and get a worse result, you have learned nothing except that you now have two unknowns. Third, keep a small notebook of settings that worked. The machine gives you infinite positions; your memory does not give you infinite recall, and re-discovering your aluminum settings every third job is how people conclude the machine is inconsistent when it is their own log that is missing.
Most problems attributed to the Ironman 240 in forums and service calls are setup problems. The recurring ones:
| Pros | Cons |
|---|---|
| 30–280 A covers 24-gauge through 1/2-inch steel | 186 lb — shop equipment, not portable gear |
| Infinite voltage and wire feed for precise arc tuning | 240V only; needs a dedicated ~50 A circuit |
| Run-in technology delivers clean, low-spatter arc starts | MIG and flux-core only — no stick or TIG |
| 60% duty at 200 A; 100% around 160 A for light work | No digital display or synergic presets |
| Geared, aluminum-housed drive system built to last | Spool gun for aluminum sold separately |
| Spool gun ready — no adapter needed | Not recommended for generator power |
| Complete package: gun, regulator, gas hose, cart, chart | Price is steep for occasional hobby use |
| 5/3/1 warranty — 5 years on the transformer | |
| Diagnostic light ends most troubleshooting guesses |
The Ironman 240 competes in the heavy-duty single-process MIG class, and its competitive position is unusual: it offers arc quality and control features associated with machines costing more, while carrying a warranty that most of them do not match. Where it gives ground is versatility and electronics. Multi-process machines in the same price band will also run stick and TIG, and premium machines add digital interfaces, pulse modes, and synergic programs. Whether those features are worth real money depends entirely on whether you use them.
The warranty comparison is the one that surprises people. Hobart’s coverage — five years on transformers, stabilizers, and main rectifiers; three years on generators, PC boards, and drive systems; one year on guns — is meaningfully longer than the industry norm for this class, and it reflects a manufacturer that expects the machine to survive its warranty period. For a machine bought as a ten-year shop tool rather than a season’s project, that asymmetry matters as much as any arc characteristic.
There is also a used-market angle worth considering. Ironman 230s and 240s come up for sale when shops close or downsize, and because the construction is transformer-based with serviceable wear parts, a well-kept used unit is not the gamble it would be with a machine whose inverter board you cannot inspect. What to check on any used Ironman: feed consistency through a full spool (worn drive rolls and tired liners show up here), thermal behavior on a long test weld (the machine should hold output and, if it is going to trip, trip cleanly with the diagnostic light rather than smelling hot), arc starts with run-in engaged, and physical condition of the gun and ground clamp — both are cheap to replace, but their state tells you how the machine was treated. A used machine selling for a fraction of new, with consumables replaced and a known history, is a legitimate way into this class if the budget does not stretch to new — and it inherits the same arc characteristics that make the new machine worth reviewing.
Against its own stable, the calculus is simpler: the Handler line exists for 120V users and lighter duty, the Ironman line for shops. There is no version of this review where a 120V hobbyist should buy an Ironman 240, and no version where a full-time fabricator should settle for a machine whose duty cycle runs out during a normal afternoon.
Purchase price is the entry fee; consumables and downtime are the real bill. The Ironman 240’s running costs are low for its class, mostly because of decisions made at design time rather than anything you do at the wire cabinet.
On longevity, the honest evidence is indirect but consistent: transformer machines of this construction have few failure modes. There is no inverter board to cook, no capacitor bank to age, no software to obsolete. The components that do wear — drive rolls, gun liner, contact tips, the fan motor — are all serviceable with hand tools and stocked parts. The 5-year transformer warranty is a manufacturer’s statement that it expects the power section to outlive the coverage period, and the 3-year coverage on PC boards and drive systems acknowledges that electronics, where present, are the shorter-lived half. A machine bought today for daily fabrication will almost certainly still be welding in ten years; the question will be which consumables it has been through, not whether it needs replacing.
Hobart backs the machine with its 5/3/1 limited warranty: five years on transformers, stabilizers, and main rectifiers; three years on generators, PC boards, and drive systems; one year on MIG guns and torches. Consumables — tips, liners, nozzles — are wear items and are not covered, which is normal and should be part of your running-cost math anyway.
Hobart Welding Products is an ITW (Illinois Tool Works) brand, manufactured in Troy, Ohio, and shares its parent company with Miller. That last fact answers one of the internet’s oldest welding arguments: people frequently ask whether Hobart is “made by Miller.” They are distinct brands with their own product lines, engineering, and dealer networks — but they do report to the same parent corporation. The practical ownership differences are in product positioning, dealer support, and price; the corporate structure is not a quality signal in either direction.
Parts and consumables availability is strong — Hobart machines are sold through welding supply houses that stock tips, liners, and drive rolls on the shelf, which matters more than it sounds when a job stops for a five-dollar part. Service support runs through the same network, with a published service line on the spec sheet.
Thirty to 280 amps of welding output, with a rated output of 200 amps at 60 percent duty cycle. Input-wise it draws about 50 amps at 240 volts at rated load — roughly 11.4 kVA — which is why it needs its own dedicated 240-volt circuit.
Plan on a dedicated 50- or 60-amp, 240-volt circuit with correctly sized wire, subject to local code and the actual run length. The machine’s input at rated load is around 50 amps at 240V, so a shared or undersized circuit will trip under load. Confirm against the nameplate and your local electrical code before installation.
Yes, with the optional SpoolRunner 200 spool gun — the machine is spool gun ready with no adapter required. The gun welds 16-gauge to 1/2-inch aluminum with .030–.035 wire. It cannot weld aluminum through the standard MIG gun; no machine can, because soft aluminum wire will not push reliably through a long liner.
It is easy to set up and operate — the settings chart and two infinite controls make configuration approachable — but it is a lot of machine and a lot of money for someone still learning puddle control. A beginner with 240V power and growth plans will not be held back by it. A beginner without either is better served by a lighter, cheaper machine until the skill justifies this one.
The 240 adds infinite voltage control, run-in arc starts, a diagnostic light, and 30 more amps over the 230’s 250-amp ceiling, while raising the 60-percent duty point from 175 to 200 amps. The 230 remains a good machine used. Choose between them on price, condition, and warranty — the arc quality of both is well regarded, and the 240’s advantages are control and self-diagnosis rather than a different kind of bead.
Hobart’s spec sheet states that running the Ironman 240 off generator power is not recommended. The machine wants clean, stable utility power, and generator output under variable welding load is neither. If generator operation is a requirement for how you work, choose a machine designed for it.
Below the rated 60 percent — the 60-percent rating applies at 200 amps, and duty falls as output rises, to roughly a third at 240 amps and lower still at maximum output. The full curve is on the machine’s duty cycle chart; the practical reading is that 280 amps is burst capability for demanding passes, while continuous work lives at 200 amps and below.
Hobart welding products are manufactured in Troy, Ohio, USA, where the brand has operated since its beginnings. Hobart is an ITW (Illinois Tool Works) brand — the same parent company as Miller, though the two remain distinct brands with separate product lines.
The shop we started with still runs two of these. One welds frames all week; the other does sheet and light work on a cart. Neither has needed anything beyond tips, liner, and the occasional nozzle. That is what a review can give you that a spec sheet cannot: what the machine is doing years after the box is gone.
The Hobart Ironman 240 is what a shop-class MIG welder should be. It has enough output to make single-pass thick welds, enough resolution in its controls to make thin ones without argument, an arc start that behaves the same way every time, and a drive system built from metal where it matters. It carries none of the electronics that add failure modes without adding weld quality, and it backs the parts that do the work with a five-year warranty.
It is also honest about its limits: 186 pounds, 240 volts, fifty amps of draw, MIG only, no generator support. Those are not flaws to forgive — they are the terms of the trade. Buy it if your work is serious and your power is ready. If either of those is not true yet, there is a machine in this catalog for that, and it is not this one.
For a machine you intend to still be welding with a decade from now, that combination of capability, control, and warranty is the whole argument.