Stick Welding Chart: The Complete Electrode, Amperage & Settings Reference (2026)
Stick welding chart guide: amperage by rod diameter, E6010 vs E7018, polarity, positions, and troubleshooting tables for SMAW…
READ ARTICLE →Years ago, early in my career, a contractor talked me into “saving the shop money” on a repair job at a public swimming pool. The failing piece was a 316 stainless handrail stanchion, the kind that gets splashed with chlorinated water forty hours a week, and the rod bin was stocked with two grades that looked almost identical once they were out of the package. I welded the broken gusset with the cheaper coil of rods nobody had labeled, ran a decent-looking bead, chipped the slag, brushed it, and went home satisfied. Fourteen months later the maintenance supervisor called. Pitting had opened along the heat-affected zone of my weld like a row of tiny rust freckles, and the rail had to come out entirely. The rod I grabbed had been 308L. The base metal demanded 316L, with its molybdenum standing guard against chloride attack. My weld looked fine. Under the surface, chemistry was already keeping score.
Stainless steel stick electrodes are flux-coated consumable rods, classified by the American Welding Society as E308L, E316L, E309L and related designations, that carry welding current through a stick holder and deposit corrosion-resistant weld metal into stainless steel joints. Each classification pairs with specific base metals: 308L for 304 stainless, 316L for 316 stainless, 309L for joining stainless to carbon steel. The flux coating shields the puddle, stabilizes the arc, shapes the bead and adds alloy elements, which is why coated electrodes work outdoors, overhead, in drafts, and in cramped spaces where bottles, feeders and torches will not fit.
That combination of portability and metallurgical precision is why stainless stick rods remain the default repair consumable in plants, on boats, in food facilities and on construction sites. This article walks through the whole discipline: how to decode markings like E316L-16, how the coating and core wire actually behave in the arc, how to choose between 308, 309, 316 and specialty grades, how rod diameter maps to amperage and plate thickness, how to weld vertical and overhead without sagging, how to store rods so moisture never sabotages the arc, how to diagnose porosity, inclusions and cracking, and where each classification earns its keep in real service. The pool handrail story ends differently when the right rod goes in the holder the first time.
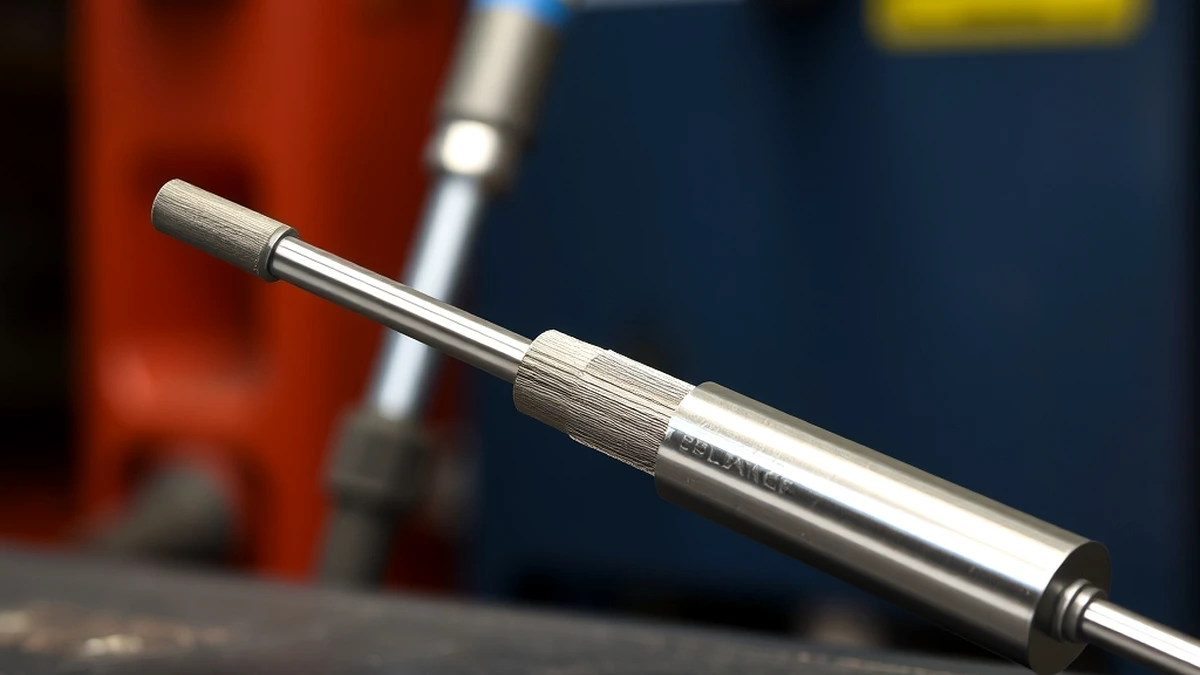
A stick electrode for stainless steel is a three-part system disguised as one piece of metal. The core wire is a drawn stainless alloy rod sized to the classification’s chemistry. Wrapped around it is the flux coating, a pressed mixture of minerals, ferroalloys and arc-stabilizing compounds that does four jobs simultaneously. And the deposited weld metal, the bead left behind after the arc consumes both, is the engineered result: stainless steel with controlled alloy content, controlled carbon and, on L-grade rods, low enough carbon to resist sensitization during the heat cycle.
The process itself is shielded metal arc welding, the oldest and simplest arc process in common use. Strike the rod against the work, establish an arc, drag or manipulate the rod along the joint while it melts away in your hand. There is no bottle to haul, no feeder to set, no liner to replace. The rod is the filler, the shield and the current path all at once. That simplicity is deceptive, because the variables that matter, alloy match, coating type, amperage, arc length, position, moisture condition, live inside the consumable and the operator’s hands rather than on a machine panel. Mild steel rod skills transfer only partly: stainless puddles run wetter, conduct heat less willingly, and remember every thermal insult in the form of tint, distortion or carbide precipitation.
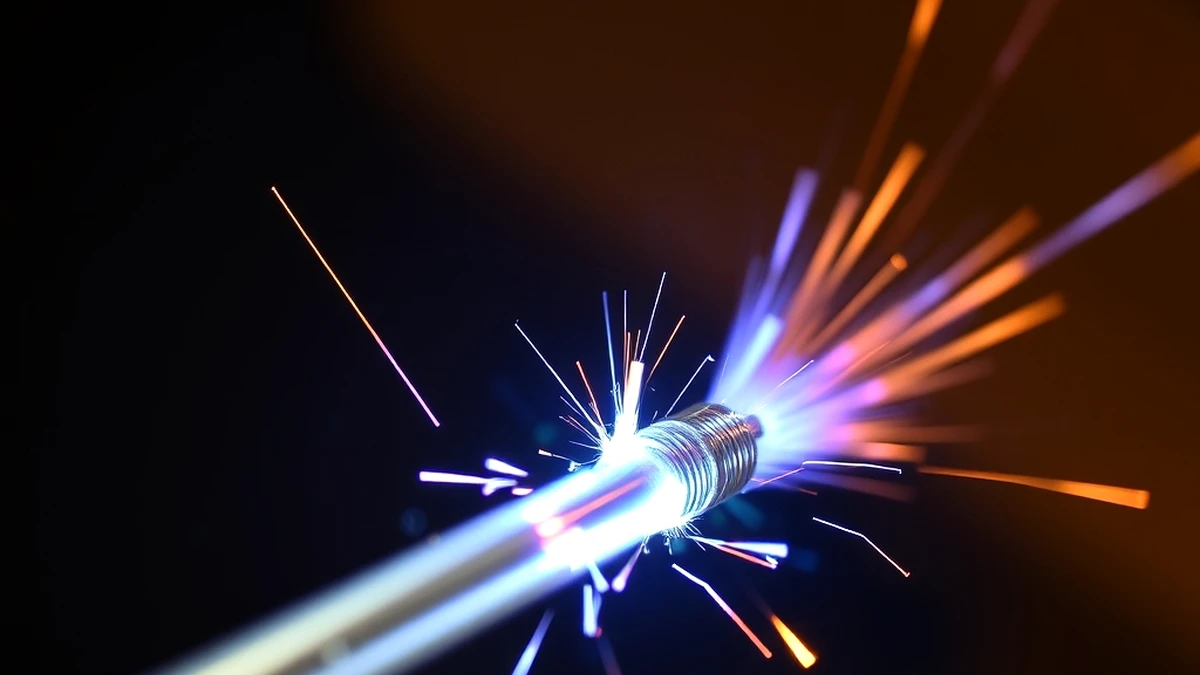
When the arc strikes, the coating on a stainless electrode burns several millimeters ahead of the arc zone, and that timing is deliberate. The forward heat drives gases out of the coating first, creating a shielding envelope before the base metal and core wire begin to melt. Then the coating melts into a slag that floats on the puddle and freezes behind it, blocking atmospheric oxygen and nitrogen from the cooling metal. Alloying powders blended into the coating, such as ferromanganese, ferrosilicon and sometimes molybdenum or nickel additions, dissolve into the weld pool to fine-tune the chemistry after dilution with the base metal.
Coating chemistry also controls arc behavior. Rutile coatings built on titanium dioxide produce a soft, smooth, easily restarted arc that beginners love; basic or low-hydrogen coatings built on calcium carbonate and calcium fluoride give a stiffer arc and cleaner, tougher weld metal at the cost of being fussier about current and polarity. Iron powder added to a coating, common in the -18 and -17 suffixes, increases deposition rate by letting part of the coating itself become weld metal. The result of all this chemistry is a consumable that manages an entire metallurgical process in the three seconds it takes to burn an inch of rod.
Three differences dominate. Puddle behavior: stainless filler wets the joint more readily than mild steel and stays fluid longer, so welders used to the stiff mild steel puddle often overwork the arc and gouge the base. Heat sensitivity: stainless conducts heat slowly and expands eagerly, which concentrates distortion near the bead and widens the visible heat tint. A bead that would look harmless on mild steel can leave a blue-gray band several rod diameters wide on stainless, and that band is oxidized surface that must be removed for corrosion service. Alloy discipline: the rod must match the base metal chemically, not just mechanically. Mild steel work forgives a wrong rod far more often than stainless work does.
There is also a practical difference at the rod box. Stainless electrodes cost several times more per pound than E6011 or E7018, they are sold in sealed packs rather than open cartons, and they carry a shelf-life consciousness that mild steel rods never demand. Treating them as a precision consumable rather than bulk supply is the first habit worth forming, and the broader welding rod types overview puts the stainless family in context with the rest of the bin.
Quick Note: Never mix rods in one container. A single 6013 dropped into a box of E308L-16 will contaminate the stainless rod it touches, and the arc will not announce which rod is which when half your bead turns out to be mild steel.
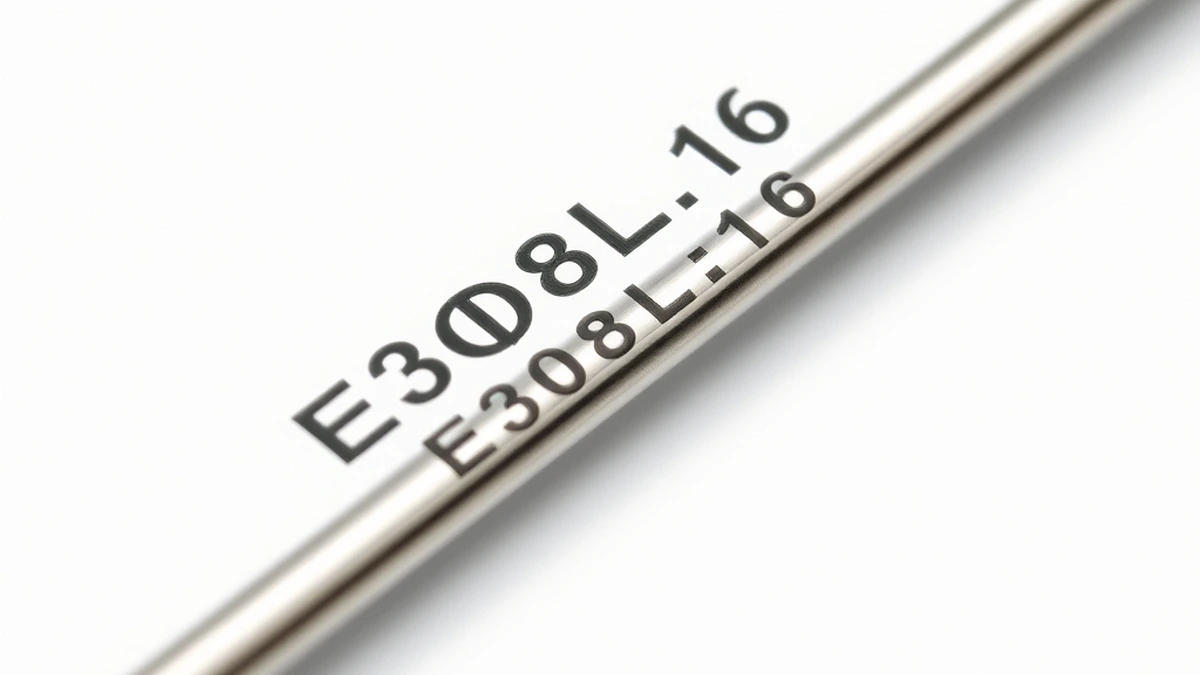
Every stainless electrode carries a stamped identification near its grip end, and the string contains more information than most welders use. Taking E316L-16 apart: the E means electrode. 316L names the deposited weld metal chemistry, the 316 family with molybdenum and low carbon below 0.04 percent. The final two digits are a coating and current group. A -16 suffix indicates a rutile-containing coating usable on both AC and direct current, with fast arc restart and a forgiving arc. A -15 suffix indicates a basic or low-hydrogen coating restricted to DC with the electrode positive, offering cleaner, tougher weld metal with a more demanding arc. A -17 suffix is a rutile-iron powder hybrid that runs even smoother than -16 and deposits faster. Some classifications carry longer suffixes such as -26, an iron-powder basic coating for flat and horizontal production work with high deposition.
Reading the suffix tells you what machine and technique the rod wants before you ever strike an arc. A welder handed a bundle of 317L-15 rods expecting to run them on an AC buzz box will be frustrated within minutes; the same person running -16 rods on a cheap AC machine will wonder why anyone pays extra for TIG. The classification system itself is defined by AWS specification A5.4 for stainless stick electrodes, published by the American Welding Society, and certified fabricators must receive rods with a test report traceable to that spec. Understanding the code is also the fastest way to become fluent in the welding rod number system that governs every stick electrode in the industry.
| Symbol | Meaning | What It Means for You |
|---|---|---|
| E | Electrode | Carries welding current |
| 308L / 316L / 309L | Weld metal chemistry | Match to base metal family |
| L (after grade) | Low carbon (< 0.04%) | Resists sensitization and intergranular corrosion |
| -15 | Basic/low-hydrogen coating, DCEP only | Cleanest weld metal, fussiest arc |
| -16 | Rutile coating, AC or DC | Forgiving all-round rod, easy restart |
| -17 | Rutile-iron powder, AC or DC | Smooth arc, higher deposition |
| -26 | Basic-iron powder, DCEP | Flat/horizontal production welding |
Important: The L in 308L and 316L is not marketing. Low-carbon fillers keep chromium from combining with carbon during the weld heat cycle, which is exactly the failure that cost that pool handrail its service life. If the base metal is an L grade, the rod should be an L grade. If the base metal is standard 304 and the part never sees heat or chlorides, plain E308 may pass; when in doubt, run the L.
Three classifications cover the overwhelming majority of stainless stick work. Learning when each belongs in the holder is the single highest-value skill in this trade, and the rest of the rod bin exists to serve edge cases around these three.
E308L deposits a weld metal that matches the composition of 304 and 304 stainless, roughly 19 percent chromium and 10 percent nickel with low carbon. It is the rod for tanks, sinks, handrails, food processing equipment, architectural trim, kitchen fabrication and general structural stainless made from the most common austenitic grade on earth. The weld offers good corrosion resistance in mild environments, excellent ductility and the familiar austenitic toughness that resists brittle failure even at cryogenic temperatures.
Where E308L fails is chloride service. Pitting and crevice corrosion attack 304-family welds in swimming pool atmospheres, coastal air, deicing salt exposure and any process fluid carrying sodium chloride. That is not a rod defect, it is base metal physics: 304 itself is the wrong alloy for those environments, and no rod can rescue it. Selection discipline starts by asking what the finished part will endure, not what the bin contains. Rod selection logic for general work mirrors the framework in how to choose a welding rod, adjusted for the stainless-specific chemistry checks.
E316L adds 2 to 3 percent molybdenum to the 308 recipe, and that addition buys resistance to pitting and crevice corrosion in chloride-bearing environments. It pairs with 316 and 316L base metal and appears on equipment in chemical processing, pharmaceutical production, marine hardware, pulp and paper, textile dyeing and any facility that washes down with chlorinated cleaners. Low carbon keeps the heat-affected zone from sensitizing, which matters on parts that will be welded, pickled and put into corrosive service.
The molybdenum makes the rod behave slightly differently at the arc too: the puddle runs a touch hotter in feel, and travel speed needs a hair more discipline to avoid a flat, washed-out bead. Amperage overlaps 308L closely for a given diameter, so machine settings transfer between the two with minor trimming. Economically, 316L costs noticeably more than 308L, which is precisely why welding a 304 part with 316L rod as a blanket “upgrade” wastes money without adding service life, while welding a 316 part with 308L rod saves little and risks everything. If molybdenum-bearing grades interest you, the alloy logic rhymes with how rod choice affects mild steel results: chemistry match beats brand loyalty every time.
E309L carries elevated chromium and nickel, around 23 percent and 13 percent, specifically to tolerate dilution. When stainless meets carbon steel, the carbon side melts into the puddle and drags the alloy percentage down; 309 starts high enough that the finished deposit still lands in the stainless range. It is the standard choice for welding stainless to mild steel, buttering a carbon flange before a stainless overlay, surfacing carbon plate with a corrosion-resistant layer, and joining stainless of unknown parentage when a 308 match cannot be confirmed.
Because of its alloy reserve, 309 also handles heat-tinted, scaled and imperfectly cleaned joints better than 308, which is why field repair crews often keep it as their general-purpose stainless rod. The tradeoff is cost and the fact that its corrosion resistance, while real, is optimized for the dilution problem rather than for chloride service. Welding over a cracked stainless casting, building up a worn shaft shoulder, or joining 304 sheet to a steel frame are all natural 309 jobs. For more on dissimilar joint behavior, the pairing notes in joining dissimilar metals cover the same shrinkage-stress concerns that show up on stainless-to-carbon joints.
Pro Tip: When the base metal cannot be identified, grind a test bead on a hidden area with a 309 rod, let it cool, and look at it. A 309 weld tolerates the unknown better than any other austenitic rod, and the test costs two inches of rod instead of a rejected assembly.
The rest of the rod bin earns its space in specific corners of the trade. E347 contains niobium, a stabilizer that ties up carbon and prevents sensitization in high-temperature service; it is the rod for exhaust manifolds, boiler components and any stainless that will live hot for years. E312, with its high alloy content and dual-phase structure, welds dissimilar metals and forgivingly handles unknown or questionable base compositions, at the cost of lower corrosion resistance. E2209 matches duplex stainless grades such as 2205, restoring the balanced austenite-ferritic structure that gives duplex its strength and chloride toughness. E385 (904L composition) serves sulfur-bearing chemical environments where 316L pitting resistance falls short. On the ferritic and martensitic side, E410 and E430 cover 400-series stainless work such as exhaust tubing and trim, usually with preheat or post-weld heat treatment requirements that austenitic rods do not carry.
None of these replace the big three in daily use, but recognizing when a job calls for one separates a fabricator from an arc operator. A refinery repair spec naming E347, a duplex plate joint called out as E2209, a stabilizer weld on an exhaust flange: each is a moment where reading the drawing pays for every hour spent studying classifications. Specialty rod guidance appears in the broader rod types and uses library, and codes on drawings usually cite the AWS classification directly, so knowing the alphabet means knowing the spec.
Selecting a stainless electrode is a filter problem. Six questions narrow the field from the whole rod bin to one box, and experienced welders run the sequence almost automatically.
Base metal composition is the first filter and the hardest to reverse. Identify the alloy before opening the box: 304 to 308L, 316 to 316L, dissimilar to 309L, stabilized grades to 347, duplex to 2209. When identification fails, a 309 rod plus a test bead is the professional fallback. Welding position comes second because not every rod runs every position; most austenitic -16 rods handle all positions, while some iron-powder production coatings are flat and horizontal only, and the package labeling will say so. Service environment shapes the chemistry requirement: chlorides push toward 316L, high heat pushes toward 347, food-contact surfaces push toward low-ferrite, polished austenitic grades, unknown or dissimilar service pushes toward 309 or 312.
Current and power source filter the coating suffix. A battery of AC-capable -16 or -17 rods suits an engine-driven machine or an old transformer buzz box; a DCEP-only -15 rod suits a modern inverter with tight current control and delivers the cleanest deposit when you have the right machine for it. Code and specification requirements may dictate the exact AWS classification, the welding procedure specification, ferrite targets and certification paperwork; on code work, the drawing and the WPS overrule personal preference. Tensile strength and mechanical requirements finish the filter: austenitic stainless weld metal typically lands around 70 to 85 ksi tensile, and if the service demands more, the joint design or alloy choice, not the rod alone, has to change. A structured take on the same decision appears in the arc welding electrode chart.
Short Note: Position and environment outrank personal preference. A rod that welds beautifully flat but cannot hold a puddle overhead will not save a job that must be welded overhead, no matter how good its corrosion numbers look on paper.
Behind every classification sits two engineering decisions: what the core wire is made of, and what the coating is made of. Both directly influence the finished weld, and understanding them explains most of the behavior welders otherwise attribute to “cheap rods” or “bad machines.”
The core wire of a stainless electrode is drawn from the same alloy families used for the base metals themselves. Austenitic wires from the 300 series dominate because they cover the majority of stainless fabrication: versatile, tough, corrosion resistant and easy to weld. Ferritic wires serve the 400 series where magnetic response, higher thermal conductivity and lower cost matter more than chloride resistance. Martensitic wires appear where hardness and wear resistance are required, and they bring the preheat and heat-treatment discipline that goes with them. Duplex wires balance austenitic and ferritic phases for strength plus chloride toughness, and they demand careful heat input control to keep the phase balance intact after cooling.
Wire chemistry must anticipate dilution. A rod welding thick stainless to thin stainless needs a composition that survives a mild dilution ratio; a rod buttering carbon steel must start with a large alloy reserve. That is why 309 exists in a slightly different chemistry than 308 even though both weld 304-family material in matched joints. Weld metal chemistry also controls ferrite content: too little ferrite invites hot cracking, too much invites embrittlement at low temperature, and rod manufacturers tune the balance for a target ferrite number typically between 5 and 15 FN for austenitic grades. Those numbers appear on mill test reports, which code work requires suppliers to provide.
The coating’s contributions are best understood as a job list. It stabilizes the arc, maintaining consistent current flow through an ionized gas column so the rod does not wander or stick. It shields the weld zone, generating gas ahead of the puddle to exclude atmospheric nitrogen and oxygen. It adds alloys, delivering deoxidizers and, on iron-powder coatings, extra deposited metal. It forms slag, trapping impurities and blanketing the bead until solidification finishes. And it controls arc force and puddle shape, which is why switching from a rutile to a basic coating on the same machine feels like changing tools entirely.
| Coating Type | Key Ingredients | Arc Behavior | Best Use |
|---|---|---|---|
| Rutile (-16) | Titanium dioxide, silicates | Soft, forgiving, easy restart | General work, out-of-position, AC machines |
| Rutile-iron (-17) | Rutile plus iron powder | Very smooth, higher deposition | Fast fabrication, all-position |
| Basic/low hydrogen (-15) | Calcium carbonate, calcium fluoride | Stiffer, deeper penetration | Critical welds, code work, soundness |
| Iron powder (-18/-26) | Iron powder with rutile or basic base | Smooth, high speed | Flat and horizontal production |
Quick Note: Basic-coated rods demand dry conditions because the coating itself absorbs moisture. Rutile rods are more tolerant. That single fact explains why a field kit usually centers on -16 rods while the shop’s critical welds run -15 rods out of a heated oven.
Every stainless rod selection is a negotiation between two axes: how well the weld resists its environment, and how much mechanical duty it must perform. They do not always point in the same direction, and the interesting engineering lives in the tradeoffs. Austenitic weld metal, the 300-family deposit from 308L and 316L, excels at corrosion resistance and low-temperature toughness but sits at a moderate tensile strength around 70 to 80 ksi. Ferritic deposits from 400-series rods bring higher thermal conductivity and lower cost with only moderate corrosion resistance. Martensitic deposits bring hardness and wear resistance with the lowest corrosion resistance of the group and a heat-treatment requirement. Duplex deposits push tensile strength above 90 ksi while retaining strong chloride resistance, but they punish excessive heat input by upsetting the phase balance.
The alloy families sort like this in practice. Austenitic (300 series): exceptional corrosion resistance, excellent ductility and toughness, non-magnetic in the annealed condition, the default for nearly all chemical, food and architectural work. Ferritic (400 series): moderate corrosion resistance, magnetic, higher thermal conductivity, lower expansion, suited to exhaust, trim and decorative applications. Martensitic: high strength and wear resistance, lower corrosion resistance, heat treatable, used for cutlery, valves and shafts. Duplex: combined austenitic-ferritic structure yielding roughly double the yield strength of plain austenite with strong resistance to stress corrosion cracking in chlorides. Matching the family to the service is the whole game; forcing a 400-series rod onto a 316 tank because it was on the shelf produces a weld that fails both tests at once.
A chemical processing plant presented a cracked fitting on a line carrying heated citric acid with trace chlorides. The base metal was 316L. The welder selected E316L-16 rods, prepped the joint by grinding back the heat-tinted edge from the original weld, and ran stringer beads at moderate amperage to keep heat input down. The molybdenum in both the base metal and the filler resisted the pitting that had started the crack, and low carbon prevented sensitization from the repair heat. A 308L rod would have welded mechanically sound and then surrendered to the chemistry within a season.
A marina repair involved a cracked bow pulpit where 316 tubing met a 304 mounting bracket, both sitting in salt spray above the waterline. This was a dissimilar joint in a chloride environment, and the choice landed on E316L for the matched portions with the understanding that the 304 bracket side was the weak link. Where brackets had to be built up heavily over a carbon steel backing plate, E309L handled the dilution. In salt-laden air, rod choice on a boat is the difference between a five-year repair and a fifteen-year repair, and the same environmental logic applies to beachfront handrails, coastal HVAC supports and dock hardware.
A food processing equipment rebuild required resurfacing a worn 304 prep table edge that would contact dairy products daily. The shop chose E308L-17 for its smooth, easily controlled arc on a fillet-type build-up, ran flat beads, and ground the finished surface to a sanitary polish. Cleanliness guided every step: fresh rods from a sealed pack, acetone wipe, dedicated stainless wire brush, no mild steel contamination anywhere in the tool chain. Corrosion resistance on food-contact surfaces is not only a chemical property, it is a hygiene requirement, because rough, pitted welds harbor bacteria that sanitation cycles cannot reach.
Pro Tip: When a weld will live in a corrosive environment, picture the maintenance crew. A bead that is ground smooth and passivated will be inspected and cleaned years later; a bead left rough and tinted will be the exact spot where the first pit appears. Finishing is part of corrosion protection, not cosmetics.
Stainless stick electrodes are manufactured in diameters from 1/16 inch up to 5/32 inch for common fabrication, with 3/16 and 1/4 available for heavy build-up and surfacing work. Diameter is a thickness decision, an amperage decision and a position decision at the same time, and choosing wrong is the fastest route to either burn-through or a cold, underfused bead that no amount of rod technique can rescue.
The working rule keeps it simple: 1/16 inch handles sheet and light tubing up to about 3/16 inch, ideal for thin-wall pipe and repair work where heat control rules. 5/64 inch covers a similar range with slightly more deposition when the joint allows it. 3/32 inch is the everyday fabrication size, comfortable from 1/8 inch up to 3/8 inch in flat and horizontal work. 1/8 inch handles 1/4 inch and heavier plate and moves large fillets quickly. 5/32 inch and above are plate and build-up sizes demanding serious amperage and usually flat or horizontal positions. The sizing framework parallels the logic behind arc welding rod size selection, with stainless adding the alloy-matching step on top.
Amperage follows diameter, position and coating. Too little current and the rod stubs, the arc wanders and fusion suffers; too much current and the puddle becomes uncontrollable, undercut bites the toes, and stainless’s heat tint spreads wide. As a starting band, 1/16-inch rods run 35 to 65 amps, 3/32-inch rods run 65 to 100 amps, 1/8-inch rods run 90 to 140 amps, and 5/32-inch rods run 120 to 180 amps. Vertical and overhead positions drop from the top of each band, typically 10 to 15 percent below flat settings, because gravity and a fluid stainless puddle both work against you. Flat and horizontal welding can use the upper band to increase deposition. Testing on scrap of the same thickness, as recommended in choosing rod size, confirms the band for your specific rod brand.
| Base Thickness | Rod Diameter | Amperage Range | Position Notes |
|---|---|---|---|
| 22 ga to 1/8 in | 1/16 in | 35 – 65 A | Any position; watch for blow-through |
| 1/16 to 3/16 in | 5/64 in | 50 – 80 A | Any position; good for sheet repair |
| 1/8 to 3/8 in | 3/32 in | 65 – 100 A | Flat, horizontal, vertical-up, overhead |
| 1/4 to 1/2 in | 1/8 in | 90 – 140 A | Flat, horizontal; vertical with care |
| 3/8 in and heavier | 5/32 in | 120 – 180 A | Mainly flat and horizontal build-up |
Standard stainless electrodes come in 10-inch and 14-inch lengths, with 12-inch common on some sizes. Longer rods mean fewer stops and higher productivity on long seams, but they also demand steadier hands because the arc length changes as the rod burns and your angle shifts. Shorter rods are easier to control in tight spaces and overhead, where a 14-inch rod becomes a long lever that wobbles. Stub loss, the unusable inch left in the holder, runs 8 to 12 percent of each rod’s weight, which is the economic argument for wire processes on production work and the reason welders on long flat seams often switch to larger diameters with higher deposition to reduce total rod count.
Size changes technique more than most welders expect. Small rods encourage short arc lengths and fine manipulation, which suits detailed sheet work and out-of-position welds where puddle control is everything. Large rods carry more current, deeper penetration and a larger, more fluid puddle that wants stringer beads and faster travel rather than intricate weaving. Overhead welding practically demands the smallest diameter the joint allows; vertical-up favors a size you can hold close to the work without fatigue. The interplay between size, position and travel is examined in thin metal arc welding techniques, and the general rod code reference explains how the stamped size relates to the certification.
Quick Note: When you change diameter, change your expectations for speed too. A 3/32 rod at 85 amps deposits metal at roughly half the rate of a 5/32 rod at 150 amps. Budget the labor accordingly instead of blaming the rod for slow progress on thick plate.
Stainless electrodes leave the manufacturer sealed, often in a foil or plastic pouch inside a carton, and that seal is the beginning of the rod’s service life rather than packaging trivia. Flux coatings, particularly basic and low-hydrogen formulations, absorb moisture from humid air. Moisture in the coating converts to hydrogen at the arc, and hydrogen dissolved in a stainless weld shows up as porosity, coarse spatter, and in restrained joints, delayed cracking hours after the bead has cooled. Dry rods and wet rods behave like different products on the same machine.
Low-hydrogen electrodes for mild steel, notably 7018, are famously baked and held in holding ovens before use, and the habit transfers to stainless -15 basic-coated rods. A rod oven held at the temperature specified by the manufacturer, commonly around 250 to 500 degrees Fahrenheit depending on the coating, keeps basic rods at their designed hydrogen level for days. Rutile -16 and -17 rods are far more tolerant, and for typical field work, simply keeping them in the sealed original pack until the moment of use is sufficient practice. The heated-oven workflow is documented from the mild steel side at homemade rod oven builds and drying rods safely, both of which translate directly to stainless basic coatings.
Field storage habits matter even more than shop habits because the field is where seals get cut open on damp mornings. Keep sealed packs in a dry box or the truck’s covered compartment, not on the floor of a humid trailer. Open only what the shift will use. Never return unused rods from a wet job to the sealed pack with the rest. If a rod has absorbed moisture, drying per the manufacturer’s published schedule can sometimes recover it; if the coating has visibly swollen, cracked or feels chalky, the rod is finished and belongs in the scrap bin, not the holder.
A workable storage standard for stainless rods covers four variables. Humidity: keep the storage area dry; a sealed cabinet with a desiccant packet protects opened packs. Temperature: store away from temperature swings that cause condensation inside packaging, especially cold shops that warm up during the day. Packaging: original sealed container until use, re-tape opened cartons, and never store rods loose where they touch each other’s coatings or pick up grinding dust. Stock rotation: first in, first out, so no box quietly ages past its useful life, and log opening dates on any pack that leaves the seal.
| Storage Factor | What Goes Wrong | Correct Practice |
|---|---|---|
| High humidity | Hydrogen pickup, porosity, cracking | Desiccant cabinet; sealed packs until use |
| Temperature swings | Condensation inside packaging | Stable, cool, covered storage |
| Loose rods | Coating damage, contamination | Keep rods in cartons or rod racks |
| Old stock | Coating degradation, arc instability | FIFO rotation with opening-date labels |
| Floor storage | Moisture wicking, physical damage | Shelf storage at least a foot up |
Contamination runs in both directions. Rods must stay clean of oil and dirt so the arc starts cleanly and the weld does not inherit carbon or hydrogen from the surface, which means clean gloves when handling and a wipe with a dry cloth if a rod has been handled bare. The rod must also not contaminate anything: a stainless rod dropped into mild steel scrap, or a mild steel rod used to tack a stainless joint, creates a repair that has to be gouged out. Welders who keep dedicated brushes, grinding wheels and even separate gloves for stainless work avoid the iron-particle contamination that causes rust staining on finished stainless surfaces weeks after delivery. Handling discipline for consumables is expanded in stick welding glove selection, since clean hands start with the right hand protection.
Important: Rust on a rod’s core wire is a disposal signal, not a cleaning project. Wire-brushing a corroded stainless rod restores its appearance and leaves the coating bond compromised and the surface chemistry dirty. The rod costs a fraction of the joint it will fail.
Stick welding’s structural advantage over every other process is position independence. Nothing feeds, nothing bottles, nothing tips: the rod reaches into a tank, under a pipe rack and up a column in any orientation the welder’s body can reach. Stainless stick electrodes inherit that freedom, with the caveat that the fluid stainless puddle needs tighter discipline than mild steel once gravity enters the picture. The universal out-of-position toolkit is short arc length, stringer beads, slightly reduced amperage, and a travel speed fast enough to freeze the puddle before it sags.
Vertical-up is the workhorse orientation for vertical grooves and uphill fillets because it lets the deposited metal build a shelf that supports the puddle. Start at the bottom of the joint, establish the arc on both edges, and move in a tight step or triangle pattern upward with a pause brief enough to tie the toes but short enough that the puddle never grows past a quarter-inch wide. Hold the rod shorter than normal, about 3/4 to 1 inch of arc length, because a long arc on vertical stainless throws the force off the joint and lets the metal run. Amperage sits at the lower end of the diameter’s band: a 3/32 rod that runs happily at 90 amps flat might prefer 75 to 80 amps overhead and vertical, because extra heat on a vertical face converts control into a cascade. Practice structures for uphill work are laid out in vertical welding drills.
The classic vertical-up failures each have a signature. A bead that is tall and lumpy means travel is too slow or the arc too long. A bead with a glassy, frozen surface and no tie-in at the toes means amperage too low. A puddle that collapses mid-pass usually means a weave was too wide or the pause at the edges too long. Correct one variable at a time on a scrap plate welded in the same position before touching the actual joint.
Overhead stainless stick welding is where the rod’s small advantages shine. Use the smallest diameter the joint allows, drop amperage into the lower third of the band, and keep arc length so short that you can hear the difference in the sound, a steady crackle rather than a soft hiss. Work in stringers, travel slightly faster than instinct suggests, and let the slag harden fully before chipping because hot stainless slag falling from overhead sticks to skin and burns through clothing. Tilt the rod so the arc force points slightly back into the joint rather than straight down, which keeps the deposited metal from hanging in a drip. Fatigue is a real hazard overhead; take breaks and stay hydrated, because a tired arm at overhead is the origin of most sagged beads.
Overhead challenges cluster into three groups: falling slag, puddle control and personal exposure. Quick-setting slag coatings, which rutile rods provide, handle the first. Short arc and stringers handle the second. A cap, jacket with no exposed neck, safety glasses under the helmet and gloves with cuffs cover the third. The horizontal and flat positions present the opposite problem, usually too much heat rather than too little: travel speed and stickout discipline keep flat beads from turning into wide, washed-out ribbons that undercut the toes.
Pro Tip: Tack the rod tips on a scrap plate before starting an overhead pass. Pre-heated rods start smoother, and the first arc of an overhead pass is the one most likely to stick to the work when everything is awkward.
The same four problems recur across positions with predictable fixes. Puddle sagging on vertical and overhead: lower amperage 10 percent, shorten arc, slow the weave, switch to stringers. Poor tie-in at the toes: hold the arc on the edges a fraction longer, verify amperage is not too low, and clean the previous pass thoroughly. Slag trapping between passes: chip, file and wire-brush every pass before the next one lands, no exceptions on stainless because the slag is glassy and stubborn. Distortion pulling the joint out of alignment: tack more densely, alternate sides, and use backstep sequences so heat does not accumulate in one region for long. A troubleshooting companion for the general case lives at arc process troubleshooting, and the fundamentals that keep positions working are the same ones taught to beginners learning the craft.
Most stainless stick welding problems announce themselves in the bead, and nearly all of them trace back to one of five variables: the wrong rod, wet or contaminated rods, wrong amperage, wrong arc length, or a dirty joint. Learning to read the evidence converts wasted rod into diagnosable data. The four defects that show up most often are porosity, slag inclusions, cracking and erratic arc behavior, and each has a short list of likely causes worth checking in order.
Porosity appears as pinholes or cavities in the finished bead. On stainless the usual culprits are moisture in the coating, oil or paint on the base metal, arc length stretched too far so shielding breaks down, or a draft blowing across an uncovered arc, though the last matters less with coated rods than with gas processes. The fix sequence is: break to a fresh sealed pack, clean the joint with acetone, shorten arc length, and verify the rod matches the job. Contamination-driven porosity also comes from grinding wheels previously used on mild steel; dedicate stainless discs and brushes and label them. The general science of gas entrapment is covered in porosity in welding.
Slag inclusions are trapped flux between passes or along a joint edge. They happen when a bead is laid over an uncleaned previous pass, when travel speed outruns the puddle and traps the advancing slag, or when a weave is so wide the slag folds into the center. Chip, file and wire-brush between passes, keep weaves within reason, and inspect the bead toes before covering them. On X-rayed work, inclusions are the defect most often traced to impatience rather than equipment.
Cracking in stainless weld metal or along the heat-affected zone usually points to chemistry or stress. Wrong filler for the base metal, heavy dilution from carbon steel, excessive restraint on a joint that shrinks freely, or an overstretched concave bead all concentrate stress in the wrong place. Grinding the crack out completely, verifying removal, and re-welding with lower heat input and the correct classification is the only fix that holds. Preheating is rarely required for austenitic stainless, but it becomes relevant for martensitic and ferritic grades and for heavy restrained sections, which is exactly the kind of nuance the AWS American Welding Society specifications encode for each classification.
| Defect | Likely Cause | Fix |
|---|---|---|
| Porosity | Moisture, dirty joint, long arc | Fresh sealed rods, acetone clean, shorten arc |
| Slag inclusion | Uncleaned pass, wide weave, fast travel | Chip and brush every pass, moderate weave |
| Cracking | Wrong filler, high restraint, concave bead | Correct rod, reduce heat input, grind and re-weld |
| Undercut | Amperage too high, travel too fast, wrong angle | Trim current, slow slightly, adjust angle |
| Hard spot | Iron contamination on stainless | Dedicated stainless tools, clean gloves |
An unstable arc on a stainless rod is rarely the rod’s fault. Work through the checklist: polarity matches the coating suffix, since basic -15 rods demand DCEP while rutile -16 runs AC or DC; current sits inside the diameter’s band, because under-current rods stick and wander while over-current rods boil and spit; connections are tight, because a corroded ground clamp or loose electrode holder drops voltage and makes the arc flicker; arc length stays roughly equal to the rod diameter, no longer; and the rod is dry, because moisture converts into a crackling, spattering arc that no machine adjustment will calm.
Spatter control follows the same audit plus travel discipline. Spatter volume climbs with excessive current, long arcs, a work angle that points the arc away from the joint root, and weaving that whips the puddle. Bringing those four back into range typically cuts spatter by most of what anti-spatter sprays would otherwise mask. Mechanical checks on the holder itself, worn grooves in the jaw that grips the rod, a cable coiled into an inductive loop, help more than welders expect; the fix list for related feed and holder complaints runs through reducing spatter systematically. Consistent work angle, consistent travel speed and a short arc remain the three cheapest quality upgrades available to any stick welder.
Quick Note: If the arc gets worse halfway through a rod, suspect the holder jaw. Oxidized or pitted jaws do not grip stainless rods cleanly, resistance climbs at exactly the point where the rod has shortened into the bad jaw zone, and the bead you were laying suddenly goes soft.
Every process has territory it owns, and stainless stick welding owns some territory that nothing else touches as conveniently. Field repair and maintenance top the list: a cracked bracket on a rooftop unit, a broken rail on a ship’s deck, a failed seam inside a tank. These jobs arrive at inconvenient angles in inconvenient weather with no room for a feeder or a bottle, and a carton of rods plus an inverter handles them. Pipe and tube work comes next, especially root passes and tie-ins on small-diameter stainless line where a rod reaches into a rack of piping that a torch cannot. Outdoor structural fabrication, from municipal stainless furniture to plant piping supports, benefits from the same wind independence that makes stick popular on carbon steel. Heavy build-up and surfacing use large-diameter rods to restore worn stainless components economically.
Industry demand shapes the rest. Food and beverage plants run stainless stick on structural supports and utilities. Chemical facilities use it for tank repairs and pipe work where procedures specify coated electrodes. Water and wastewater treatment relies on it for stainless handrails and equipment frames in damp, chloride-tinged atmospheres. Marine fabrication keeps it for hardware repair at the dock. Even the power sector uses stainless stick for boiler and turbine component repairs with specialty classifications. Workload planning for shops that chase this business assumes rod skills first, because the machine is cheap and the knowledge is not; the shop’s carbon steel side, covered from the mild steel angle at 7018 rod applications, often shares the same operators and equipment.
Short Note: Pipe work is where stainless stick repays study fastest. Root pass quality decides the weld, small diameters and open roots are routine, and a welder who can run a consistent root with a 1/16 or 5/64 rod is worth considerably more than one who can only fill.
Stainless can be welded by SMAW, GTAW, GMAW and FCAW, and the honest answer about which to use is “it depends on the constraint that binds hardest.” Stick wins when portability, position access or wind dominate the job. TIG wins on thin material, visible product welds and root passes that must be perfect. MIG wins on clean production work with a bottle handy and short-circuit settings tuned for sheet. Flux core wire wins on long outdoor seams where deposition speed matters; the wire side of that comparison is developed fully at stainless flux core wire welding.
| Constraint | Best Stainless Process | Why |
|---|---|---|
| No power or extreme remoteness | Stick | One holder, rods, engine drive |
| Wind or drafts | Stick or gasless flux core | Coating/built-in shielding unaffected |
| Tight quarters, odd positions | Stick | Rod reaches anywhere the hand fits |
| Thin sheet, heat control | TIG | Pedal control, small fusion zone |
| Visible, polished seams | TIG | Cleanest as-welded appearance |
| Long outdoor seams | Flux core wire | Continuous feed, high deposition |
| Dirty or scaled base metal | Stick | Arc tolerates imperfect prep best |
Many repair welders standardize on stick for everything stainless because the decision cost is low: no settings to debate, no consumables beyond rods and gloves, and one machine that also welds carbon steel, aluminum with the right rod, and runs on a generator if necessary. Generator compatibility matters more than people plan for; sites that require stick welding on a generator need amperage headroom most small sets cannot provide, which is a spec-check worth doing before the truck is loaded. The broader process comparison appears in stick versus MIG and MIG, TIG and stick compared, while spec-driven rod selection for mild steel jobs is outlined at rod choices for fence pipe.
A maintenance welder named Priya got called to a bottling line at 11 p.m. after a stainless guide rail sheared off its mounting plate mid-shift. The rail is 304, the mounting plate is 304, the plant runs two shifts and every hour of downtime costs real money. She could not bring a cart between the conveyors, the floor was wet from the washdown that had just finished, and the joint sat four inches off the deck in a gap too narrow for a TIG torch. She pulled a stick holder and a sealed pack of 308L-16, set the inverter to roughly 85 amps for a 3/32 rod, crouched into the gap and welded a small fillet on each side in about eleven minutes. After chipping and brushing, she wipe-checked for tint, filed the bead toes smooth so sanitation would not flag a rough edge, and the line restarted before the shift change. Nothing about that job favored a fancier process. Access, weather and speed all favored the rod.
The second story is a warning about codes rather than technique. A fabricator building stainless handrail for a municipal project received an inspection callback because the welder had used E308L where the specification called out E316L, reasoning that the visual difference was nil and the environment was “just outdoors.” The inspector was not interested in the reasoning: the drawing named the classification, the test report had to match the drawing, and every bead of that rail was gouged out and replaced. Classification discipline is cheap insurance. The same professional habit that reads a rod stamp before striking an arc also reads a drawing before loading the truck, and the project documentation habits around that discipline start with reading welding blueprints.
Important: On code and public-works work, rod packaging goes in the job file. Mill test reports, lot numbers and AWS certification paperwork prove compliance after the fact, and a welder who tosses the carton loses the only evidence that the right rod was used.
Coated rod technology moves more slowly than wire processes, but the advances of the past two decades are real and mostly invisible to the casual user. More consistent extrusion means tighter coating thickness around the core wire, which shows up as steadier arc force from the first inch of the rod to the last. Improved powder blends give better arc starting in cold, damp conditions, a direct answer to field complaints about rods that stick on the first strike. Iron-powder coatings with higher loading push deposition rates upward on flat and horizontal work without sacrificing the all-position variants that remain available. Low-ferrite formulations give fabricators tighter control over ferrite number, which matters for specs that call for a target FN range rather than a loose “some ferrite present.”
Equipment has evolved alongside consumables. Modern inverters deliver precise current control with hot-start and arc-force assists that make basic rods forgiving on a machine that would have struggled a decade ago. Some machines offer AC output tuned specifically for stable rutile rod operation, widening field options where only AC engine drives are available. Looking forward, electrode development is pulling in three directions: lower-emission coatings designed to reduce fume generation at the arc, part of the industry’s response to tightening exposure rules; smarter process integration where the power source remembers rod-specific parameter sets and the operator selects a program rather than dialing; and advanced coating science, including nano-structured additives that manufacturers are trialing for arc stability and slag release. Regulatory pressure shapes the fume side of that roadmap, with OSHA’s welding safety resources and NIOSH welding research tracking exposure data that informs both coating chemistry and ventilation practice. Safety infrastructure for stainless work generally is framed by federal welding standards, with the underlying regulation text hosted at eCFR 1910.252.
Quick Note: New coating batches arc differently than the old favorite. When a trusted rod brand changes generation, run a fresh test bead before starting production, and expect to trim amperage by a few amps in either direction.
A practical kit for someone who welds stainless regularly looks smaller than the rod catalog suggests. The sequence below gets a welder productive without overbuying.
With that kit, a welder can walk onto nearly any stainless repair and make a sound, correctly classified weld without a second trip to the supplier. The economics favor the discipline: rods cost more than the mild steel version, but the failed weld costs far more than either, and fume management on stainless work protects the person holding the stinger for a full career. Broader health context for the trade sits at are welding fumes toxic, and strength expectations for finished joints are discussed at how strong a weld really is.
Pro Tip: Keep a one-page log per job: rod classification, lot number, diameter, amperage, polarity, position. It takes ten seconds per rod change and settles every question that inspection, rework or warranty ever asks.
What are stainless steel stick electrodes used for? They weld stainless steel with a stick holder and arc: food and chemical equipment, tanks, piping, handrails, marine hardware, exhaust components, structural stainless and field repairs. The flux coating provides shielding, so no gas bottle is required, and the classification is chosen to match the base metal and service environment.
Which rod do I need for 304 stainless? E308L is the standard match for 304 and 304L. Choose the L grade to keep carbon low and avoid sensitization, and confirm the coating suffix suits your machine: -16 for AC or DC versatility, -15 for DCEP only with the cleanest deposit, -17 for a smooth high-deposition option.
Which rod for 316 stainless or chloride environments? E316L, because the molybdenum content resists pitting and crevice corrosion in chlorides. That covers chemical plants, marine exposure, pool areas and any equipment washed down with chlorinated cleaners.
What size stainless rod should I use? Match diameter to thickness: 1/16 inch for sheet up to about 3/16 inch, 3/32 inch for the everyday 1/8 to 3/8 inch range, 1/8 inch for 1/4 inch and heavier, 5/32 inch for thick plate build-up. Then set amperage within that diameter’s band, dropping 10 to 15 percent for vertical and overhead.
Do stainless rods need to be stored differently from mild steel rods? Yes. Keep them in the sealed original packaging until use, store in a dry cabinet away from humidity and temperature swings, rotate stock first-in first-out, and for basic low-hydrogen coatings, hold them in a rod oven at the manufacturer’s specified temperature. Moisture in the coating causes porosity and cracking.
Can I weld stainless stick outdoors in wind? Yes. The coating generates its own shielding, so drafts affect the arc far less than they affect gas-shielded processes. Keep the joint dry and shielded from rain, and manage fumes so they do not accumulate in the welder’s breathing zone.
Why is my stainless rod sticking and sputtering? Check polarity against the coating suffix, confirm amperage is inside the diameter’s band, inspect the holder jaws for pitting, verify the ground clamp is tight and clean, shorten arc length to about one rod diameter, and swap to a fresh sealed pack if the current rods have absorbed moisture.
Stainless steel stick electrodes remain the most dependable consumable in the stainless welder’s cabinet because they combine metallurgical precision with total portability. The classification stamp tells you exactly which alloy you are depositing, the coating delivers shielding and arc control from a sealed package, and a rod and a holder will weld anywhere a human can reach. The craft lies in the details surrounding that simplicity: reading the stamp against the base metal, matching diameter and amperage to thickness and position, keeping rods dry so hydrogen never enters the equation, cleaning between passes so slag stays where it belongs, and finishing welds so corrosion has nowhere to start.
Build the kit around E308L, E316L and E309L, learn each one’s behavior at the arc, log the settings that work, and let drawings and service conditions decide which box gets opened. Do that consistently and the failures that plague careless stainless work, pitting from a mismatched rod, cracking from wet coating, rework from a spec violation, never get a foothold. The rod is simple. The discipline is the job.